
How to Read an Edge Crush Test Chart When Specifying Corrugated Shipping Cases
A shipping case can look adequate on a packing bench and still fail after it becomes the bottom carton in a warehouse stack. Corners soften, panels bow, flaps open, or the box loses enough rigidity that a small impact damages the product inside. When this happens, the first question is often whether the selected board grade was too light. An edge crush test chart helps answer that question, but only when it is read as part of a complete case-performance decision rather than as a simple “higher number is always better” scale.
The direct interpretation is straightforward: an ECT rating indicates the edgewise compression strength of corrugated board. A higher rating generally supports a stronger box wall and a higher potential stacking load. Yet an ECT chart does not, by itself, tell you what a finished shipping case will safely carry. Case dimensions, board construction, moisture exposure, closure design, pallet pattern, handling conditions, and the duration of storage all affect the result. The practical task is to convert a board rating into a case specification that fits the actual distribution risk.
Start with what the chart is actually measuring
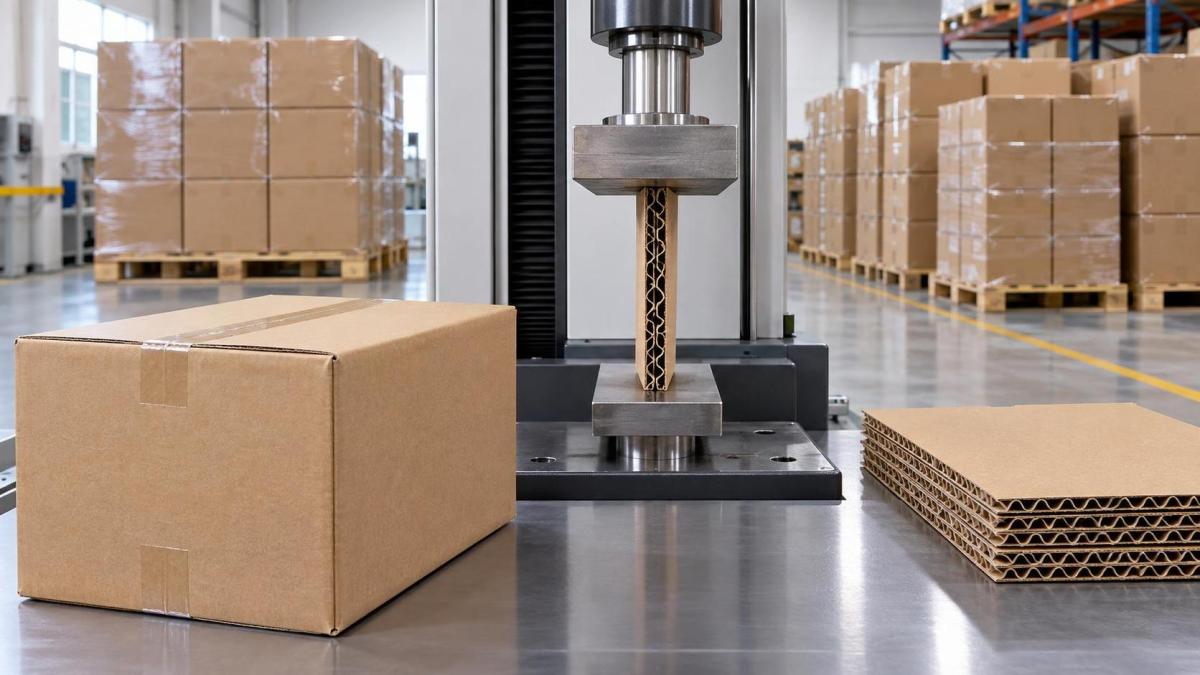
ECT stands for Edge Crush Test. In the test, a prepared sample of corrugated board is placed on edge between compression platens and loaded until it crushes. The result is commonly expressed as force per unit width, such as pounds per inch in customary U.S. packaging specifications. It measures how well the board resists being compressed through its thickness at the edge.
This characteristic matters because a closed regular slotted container carries much of a vertical stacking load through its vertical panels and corners. When cartons are stacked, the board around the perimeter acts as a structural column system. Better edgewise compression resistance usually gives the finished case more resistance to buckling and collapse.
An ECT chart may list values such as 23 ECT, 26 ECT, 29 ECT, 32 ECT, 40 ECT, 44 ECT, or higher grades. These numbers are board-performance ratings, not universal descriptions of flute type, paper weight, wall thickness, or product weight capacity. Two boards with the same ECT rating can differ in caliper, flute profile, liner composition, print surface, puncture resistance, and performance under humid conditions.
A useful reading habit is to treat the ECT value as the starting strength input. The remaining entries on the specification—outside dimensions, style, flute, joint type, print and coating requirements, storage environment, and closure method—determine whether that input becomes dependable shipping performance.
Read the rating in the context of the finished case
Suppose a team is specifying a corrugated shipper for a product that will move from production to a distribution center, remain palletized, and then travel through parcel or mixed-load channels. Selecting a board solely because its ECT number is higher than the current grade can create unnecessary cost without solving the real failure mode. Conversely, selecting a lower-cost grade based only on product weight can overlook the stacking load imposed by cartons above it.
To interpret a rating correctly, first identify the load the box must withstand. The product’s gross weight is only one part of that load. The bottom case in a stack may support the weight of several other cases, plus dynamic loads created during transport and warehouse handling. The length of time under compression also matters. A carton that survives a short internal movement may gradually lose compression strength during extended storage, especially where humidity is elevated.
Case compression performance is often estimated with empirical relationships that combine ECT with the box perimeter and board thickness. The best-known approach is commonly called the McKee relationship. It illustrates an important principle: a higher ECT board can increase predicted box compression strength, but box geometry and caliper are also significant. A large-perimeter case made from the same board may not perform like a smaller case, and a change in flute construction can change the compression result even if the nominal ECT grade appears similar.
Use such equations for preliminary specification work, not as a substitute for validating the actual converted case. Die-cut openings, hand holes, score quality, seam design, printing coverage, and the packing method can all reduce real-world strength compared with a theoretical estimate.
Do not confuse ECT with burst strength
One recurring source of specification errors is the assumption that ECT and burst, sometimes called Mullen, measure the same property. They do not. Burst testing evaluates the resistance of board to rupture under pressure applied to its surface. ECT evaluates edgewise compression resistance. Both may be relevant to package durability, but they address different failure mechanisms.
A case carrying heavy pallet stacking loads usually requires careful attention to ECT because vertical compression is central to the risk. A package likely to face puncture, rough manual handling, or abrasive contents may need additional consideration of surface durability, puncture resistance, liner quality, or other material characteristics. Replacing a burst-based specification with an ECT grade without reviewing the distribution hazards can leave an important risk unaddressed.
The same caution applies to single-wall, double-wall, and triple-wall boards. Wall construction changes the board’s thickness and structural behavior. A double-wall case is not automatically appropriate merely because the shipment is heavy; it may be selected because the required stacking load, case size, handling exposure, product geometry, or cushioning demand justifies it. The chart rating should be read alongside the complete board description.
A practical sequence for choosing an ECT grade
Specification work becomes more reliable when quality and safety teams gather the operating conditions before comparing chart values. Begin with the actual shipping unit rather than with an inherited board grade from a different product line.
- Define gross case weight. Include the product, interior packaging, inserts, labels, and any retained packaging components. Do not use net product weight when the shipping case is what must be supported.
- Record outside case dimensions and style. Measure the finished shipping case, since perimeter and depth influence compression behavior. Note whether it is a regular slotted container, full-overlap design, tray, die-cut mailer, or another style with different load paths.
- Map the distribution route. Identify pallet stacking, warehouse dwell time, unit-load configuration, manual handling, conveyor transfer, parcel movement, and likely side loading. A case used only in a controlled internal flow has different demands from one exposed to repeated carrier handling.
- Establish the worst credible stack condition. Consider how many cases may be above the lowest carton, whether pallets may be double stacked, and whether load concentration from overhanging or misaligned cartons is possible.
- Account for environmental loss. Corrugated board can lose stiffness and compression strength when exposed to moisture. Cold-chain condensation, unconditioned storage, tropical routes, and wet loading areas should not be treated as minor details.
- Select a preliminary board grade. Use the ECT chart with the case geometry and expected load to identify a reasonable starting point. Confirm whether the needed grade is available in the desired flute and converting format.
- Validate the converted package. Test representative, conditioned cases with the intended contents and closure method. Review compression performance and inspect panels, scores, seams, and corners after testing.
This process avoids a common shortcut: taking a stated product weight, finding a seemingly corresponding line on an ECT chart, and assuming the work is complete. Charts can be useful purchasing tools, but their simplified weight guidance may assume particular case dimensions, handling conditions, or safety margins that do not match a specific operation.
Where the chart can lead to the wrong decision
Using product weight instead of stacking demand
A compact carton may hold a modest product weight but still spend time beneath a tall pallet load. In that condition, compression demand can exceed what the contents alone suggest. The lower cases need a board and structural design that account for the load above them. Conversely, a heavy item shipped one-high in a reinforced unit load may have a different governing risk, such as puncture, concentrated loading, or closure failure.
Ignoring box proportions
Long, shallow, or unusually large cases may behave differently from more compact cartons. Panel span, perimeter, and the location of scores affect how the walls buckle. A board grade that performs satisfactorily in a small standard shipper should not be copied automatically to a larger case with the same gross weight.
Assuming the specified rating survives conversion unchanged
Corrugated board can be weakened by poor scoring, excessive crushing at folds, damaged flutes, unsuitable die-cut settings, and handling before packing. Heavy ink coverage, coatings, or laminations may also influence how the board folds and how moisture moves through the structure. Incoming-board controls and converting-process checks are therefore part of ECT-based quality assurance, not separate concerns.
Overlooking openings and design features
Hand holes, ventilation cutouts, display windows, perforations, and large access features interrupt the box wall. They can be necessary, but they remove material from areas that may carry compression load. Their placement, reinforcement, and proximity to corners should be reviewed before relying on a chart-based strength estimate.
How to write a usable shipping-case specification
A purchase specification should make it difficult to substitute an apparently similar but structurally different board. Listing only “32 ECT carton,” for example, leaves critical questions unanswered. A more functional specification identifies the required edge crush rating, wall construction or flute profile where relevant, finished inside dimensions, case style, joint and closure requirements, print or coating limits that matter to performance, and any exposure conditions the package must tolerate.
It should also distinguish between a board qualification value and a finished-case acceptance requirement. The first controls the material. The second confirms that converted boxes, with their actual scores, seams, and design features, meet the intended performance level. Where stacking is safety-critical or the route is severe, a case compression test on conditioned samples provides much more meaningful evidence than a board rating alone.
For consistency, document how samples are conditioned, how cases are packed or simulated during testing, the orientation used in compression, and the acceptance criteria. A compression result from an empty, dry case may not represent a packed case exposed to the humidity and closure conditions of routine shipment.
Interpreting an edge crush test chart during quality review
When reviewing incoming materials or a proposed cost reduction, ask a narrow set of questions before approving a grade change: Is the listed ECT value equivalent to the current requirement? Is the wall construction changing? Are finished dimensions, case style, openings, and closure method unchanged? Will the route, stacking configuration, or storage duration remain the same? Has the replacement been verified on the converted case rather than only on a board sample?
A “yes” to the first question does not automatically settle the rest. For example, a comparable ECT rating in a different flute may alter caliper, cushioning, printability, and the way the case behaves around scores. The right choice may still be acceptable, but it requires a case-level review rather than an assumption based on one number.
The most useful edge crush test chart is therefore one used with disciplined inputs: real gross weight, actual box geometry, realistic stack conditions, expected humidity, and confirmation testing. Read that way, it becomes a practical control for balancing material use against shipping protection, while keeping the package specification tied to the loads the case will truly face.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
