How to Vet a Retail Packaging Equipment Supplier for Format Range and Service
Choosing a retail packaging equipment supplier is more than comparing machine prices. Procurement teams must verify whether a supplier can support the required format range—from compact cosmetic cartons to complex retail displays—while delivering reliable installation, spare parts, training, and responsive service. A line that looks impressive in a demonstration can still become an expensive bottleneck if it struggles with the substrates, carton geometries, changeover frequency, or service realities of daily production.
For buyers responsible for capital equipment, the central question is not simply, “Can this machine run our current job?” It is, “Can this supplier support the mix of work we expect over the next five to ten years, at a total operating cost we can defend?” That distinction matters in an environment where SKU counts are rising, retailers demand more shelf-ready packaging, and brand owners expect short runs without sacrificing finish quality.
Start with the work you actually need to produce
Supplier conversations often begin with a machine model and a headline speed. A better procurement process begins with a job map. Collect a representative sample of present and expected production: carton blanks, board grades, coated and uncoated stocks, windowed cartons, small pharmaceutical-style boxes, heavy-duty retail sleeves, promotional packs, and point-of-sale displays. Include the troublesome jobs, not only the easy ones.
For each sample, document the dimensions, caliper, grain direction, print coverage, die-cut complexity, glue pattern, batch size, acceptable waste level, and target output. If the equipment will sit after an offset press or digital press, also note registration tolerance, varnish type, curing method, and the condition of sheets arriving at the converting stage. A folder gluer that performs smoothly on flat, stable board may behave very differently with heavily inked sheets, curled substrates, or challenging reverse folds.
Format range should be understood as a production capability, not a number in a brochure. A stated maximum sheet size does not automatically mean the equipment can efficiently process oversized display work. Likewise, a minimum carton size may be technically possible but impractical if operators must use special carriers, run at reduced speed, or make delicate manual adjustments.
Questions that expose the real format envelope
- What are the proven minimum and maximum blank sizes for the exact carton styles we run?
- Which formats can operate at normal commercial speeds, and which require reduced-speed or optional configurations?
- What board thickness, flute profile, and coated-stock range has been validated?
- Can the line handle straight-line, crash-lock bottom, four- and six-corner, sleeve, partition, and display formats without excessive auxiliary equipment?
- How long does a realistic changeover take between our most common formats?
- What tooling, carriers, rails, glue systems, or software options are required for the claimed range?
A supplier that answers these questions precisely is usually more valuable than one offering broad but vague assurances. Ask for limitations in writing. Every converting platform has them; the risk lies in discovering them after commissioning.
Ask for proof through representative trials, not generic demonstrations
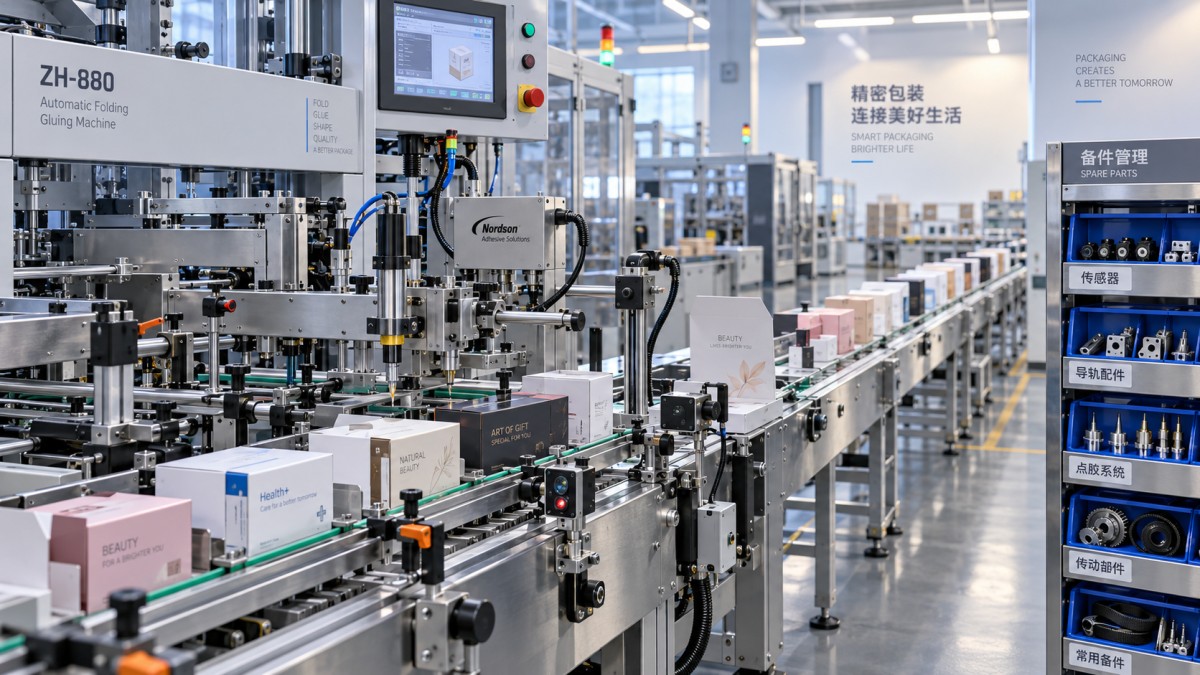
The factory acceptance test is where format claims become measurable. Whenever the project value and production risk justify it, send your own substrates and job files to the proposed supplier. A good trial should include a standard job, a difficult job, and a changeover. Watching a machine run one ideal blank for twenty minutes reveals little about its behavior across a real shift.
For die-cutting equipment, evaluate stripping quality, nick consistency, blank delivery, make-ready time, registration behavior, and waste handling. For folder gluers, inspect fold accuracy, glue placement, compression, squareness, and the stability of finished cartons at different speeds. For corrugated and retail-display applications, assess board handling, warp sensitivity, feeder performance, and whether the line preserves the visual quality required for shelf-facing packaging.
Procurement should define acceptance criteria before the trial begins. These may include dimensional tolerances, defect thresholds, speed bands by format family, setup time, output quality, and the number of acceptable units produced after startup. Avoid a single “maximum speed” condition as the sole performance measure. Commercial production depends on net output: good units delivered after setup, adjustments, stoppages, and quality checks.
Also look beyond the main machine. A high-speed die-cutter or folder gluer can be constrained by feeder logistics, pre-feeding, inspection, packing, palletizing, or data handoff from the prepress workflow. The best retail packaging equipment supplier will discuss the line as a connected production system, not isolate its own machine from every upstream and downstream issue.
Service capability is part of the equipment specification
When evaluating capital equipment, buyers often separate technical capability from after-sales service. In practice, they are inseparable. A machine with advanced motion control, servo-driven sections, camera inspection, glue monitoring, or automated setup may improve consistency—but it also needs service personnel who can diagnose electrical, mechanical, software, and process issues in a disciplined way.
Ask the supplier where its field engineers are based, which time zones they cover, and whether they directly employ technicians or rely on third-party agents. Neither model is automatically superior, but responsibility must be clear. A distributor with strong local engineers and stocked parts may be more useful than a distant manufacturer with an impressive global brand but limited regional coverage.
Request the service escalation process. Who receives the first call? What information must your team provide? When can remote diagnostics begin? At what point is an on-site visit authorized? For operations running around the clock, confirm whether support is available outside normal office hours and whether language support aligns with the plant team.
Do not overlook installation and operator adoption
Commissioning is not complete when the machine produces its first acceptable carton. It is complete when your operators, maintenance team, and production planners can run it predictably without permanent dependence on supplier personnel. Training should cover normal operation, format setup, safety procedures, fault recovery, basic preventive maintenance, quality inspection, recipe management, and escalation boundaries.
Ask how training is structured: classroom instruction, hands-on work at the supplier’s site, on-site start-up coaching, digital manuals, or refresher sessions after several months of production. The last element is especially useful. Teams often understand the equipment differently after handling real commercial orders, and a follow-up session can address the recurring issues that were not visible during initial commissioning.
For facilities pursuing greater automation, clarify who owns the integration work. Interfaces with MIS, MES, barcode systems, inspection cameras, robotic pack-out, and production reporting can create major value, but they also create accountability gaps if the scope is unclear. Define data formats, connection points, test responsibilities, cyber-access rules, and acceptance milestones in the purchase agreement.
Compare lifecycle cost instead of purchase price alone
The quoted price is visible. The cost of downtime, waste, labor intensity, energy use, tooling, and delayed spare parts is usually less visible—but often more consequential. A disciplined buyer should build a total cost of ownership model that reflects the expected job mix rather than an abstract annual volume.
Include installation, foundation or utility requirements, freight, commissioning, training, consumables, recommended spare-parts packages, tooling, software licenses, service contracts, and expected maintenance labor. For folding and gluing, factor in adhesive consumption and the consequences of glue failure. For printing and die-cutting, consider setup waste, registration losses, tooling wear, and the cost of maintaining color and cut quality across repeat orders.
It is also worth calculating the value of flexibility. A lower-cost machine may be attractive for a narrow carton range, yet expensive if growing demand brings smaller lots, more frequent artwork changes, retail-ready displays, or premium finishes. Conversely, paying for every conceivable format option can burden a plant with complexity it will rarely use. The right investment is not the widest specification; it is the capability range that matches a credible commercial plan.
Verify spare parts policy before a breakdown makes it urgent
Every supplier says parts are available. Procurement needs to know which parts are stocked, where they are stocked, how orders are prioritized, and what lead times apply to critical components. Separate commonly replaced consumables from high-risk items such as drives, control boards, servo motors, sensors, pumps, gearboxes, specialty belts, and safety components.
Ask the supplier to recommend a site spare-parts inventory for the first two years. Then challenge the recommendation against your production schedule and local supply-chain conditions. A plant far from the supplier’s regional warehouse may need a larger initial package. The cost can feel uncomfortable during procurement, but a single extended shutdown may cost more than a well-chosen inventory of critical parts.
Software support deserves equal attention. Confirm version-control practices, backup procedures, access rights, remote-service permissions, and the policy for obsolete hardware. If the line uses proprietary controls or licensed optimization software, determine what happens when the contract ends or a component family is discontinued.
Use references to investigate the supplier’s behavior under pressure
Reference calls should not be ceremonial. Speak with plants that run a similar mix of packaging formats, ideally in your region or under comparable operating conditions. Ask what happened during installation, how closely actual changeover and output matched expectations, whether service response was consistent, and which costs surprised them after purchase.
The most revealing question is simple: “What would you put into the contract differently if you bought this line again?” Experienced users often identify missing training hours, overlooked options, unrealistic spare-parts assumptions, or ambiguity around integration. Their answers can improve your specification before negotiations are finalized.
It may also be useful to ask whether the supplier communicates honestly when a job is outside the equipment’s comfort zone. In packaging production, credibility is shown not by claiming every carton is easy, but by identifying when a special feeder, revised blank design, alternative adhesive, or different machine configuration is needed.
Turn supplier evaluation into a weighted decision, not a sales impression
A formal scorecard helps prevent a polished demonstration or an attractive discount from dominating the decision. Weight the categories according to your plant’s priorities. A high-mix carton producer may give format flexibility and changeover performance greater weight. A volume operation running standardized retail sleeves may prioritize uptime, automation, and maintenance simplicity.
What should appear in the final purchase agreement
The purchase order should translate sales discussions into testable obligations. Include the exact configuration, approved drawings, utilities, interfaces, included accessories, and identified format families. State the factory and site acceptance tests, the materials to be used, the performance criteria, and the process for resolving a failed test. If a claimed capability depends on optional tooling or a special module, list it explicitly.
Service terms should identify warranty coverage, exclusions, remote-support conditions, on-site labor rates after warranty, parts availability expectations, and documentation deliverables. Require electrical diagrams, mechanical manuals, maintenance schedules, spare-parts lists, software backups where appropriate, and training records. These details may seem administrative when the project is moving quickly; later, they become the operating foundation of the line.
For procurement teams buying equipment across print, converting, corrugated, or woodworking-adjacent packaging operations, the same principle holds: process knowledge is as important as machinery. The equipment must respect the physics of the material—paper fiber, ink, coating, adhesive, board stiffness, and cut geometry—while fitting the commercial rhythm of the plant.
A capable retail packaging equipment supplier does not merely sell a press, die-cutter, folder gluer, or automated packaging cell. It helps the buyer define the practical operating window, exposes trade-offs early, and provides the technical continuity needed after installation. Vet format range through real jobs, examine service as rigorously as machine design, and evaluate cost over the life of the asset. That is how procurement turns a capital purchase into reliable packaging capacity rather than a costly production gamble.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
