What Packaging Analysis Reveals About Board Grade, Strength, and Total Cost
Corrugated industry packaging analysis is most useful when it answers a practical question: does the supplied board provide the protection the distribution cycle requires, or is the specification paying for paper, conversion effort, and warehouse space that the pack does not need?
A corrugated box can look acceptable on a receiving dock and still be a weak technical choice. It may have adequate flat crush resistance but poor stack performance after humid storage. It may use a nominally heavier board while losing strength at scores, handles, or poorly supported panels. It may pass a sample test yet create excess material consumption when repeated across high-volume production. A sound analysis connects board construction, box geometry, handling conditions, conversion quality, and delivered cost rather than treating any one test result as the whole answer.
Board grade is a construction decision, not a strength label
Board grade is often discussed as though it were a single ranking from light to heavy. In practice, it is a combination of liners, corrugating medium, flute profile, adhesive bond, moisture condition, and manufacturing consistency. Two boards with a similar basis weight can behave very differently because their paper composition and flute structure distribute load differently.
The outer and inner liners form the faces of the corrugated structure. They resist surface damage, contribute to bending stiffness, support print or label application, and carry much of the compressive load once a box is erected. The medium creates the fluted web between them. Its geometry separates the liners and provides the structure that makes corrugated board efficient: a relatively low mass can achieve useful stiffness because the faces are held apart.
A technical review should therefore start with the actual board build, not only a commercial grade name. Record the liner arrangement, medium, flute type, nominal caliper, and any special surface or moisture requirements. Then compare that construction with the job’s failure modes. A small, dense product may mainly require puncture and local impact resistance. A large lightweight appliance may depend more on panel stiffness and stacking strength. A fresh or chilled product may require performance that remains stable under elevated humidity, where paper-based strength can change materially.
It is also important to distinguish board grade from box grade. A strong sheet can become a mediocre shipping case if the die-cut pattern removes too much supporting material, if the box has long unsupported panels, or if the joint is poorly formed. Procurement language that specifies only “double-wall” or “heavy-duty board” leaves too much of this risk unresolved.
Read strength results in the context of how the box fails
Compression metrics, edgewise tests, flat crush tests, burst-oriented indicators, and puncture assessments all describe a part of performance. They should not be used interchangeably. The relevant question is not which number is highest; it is which property is most closely related to the expected transport and storage stresses.
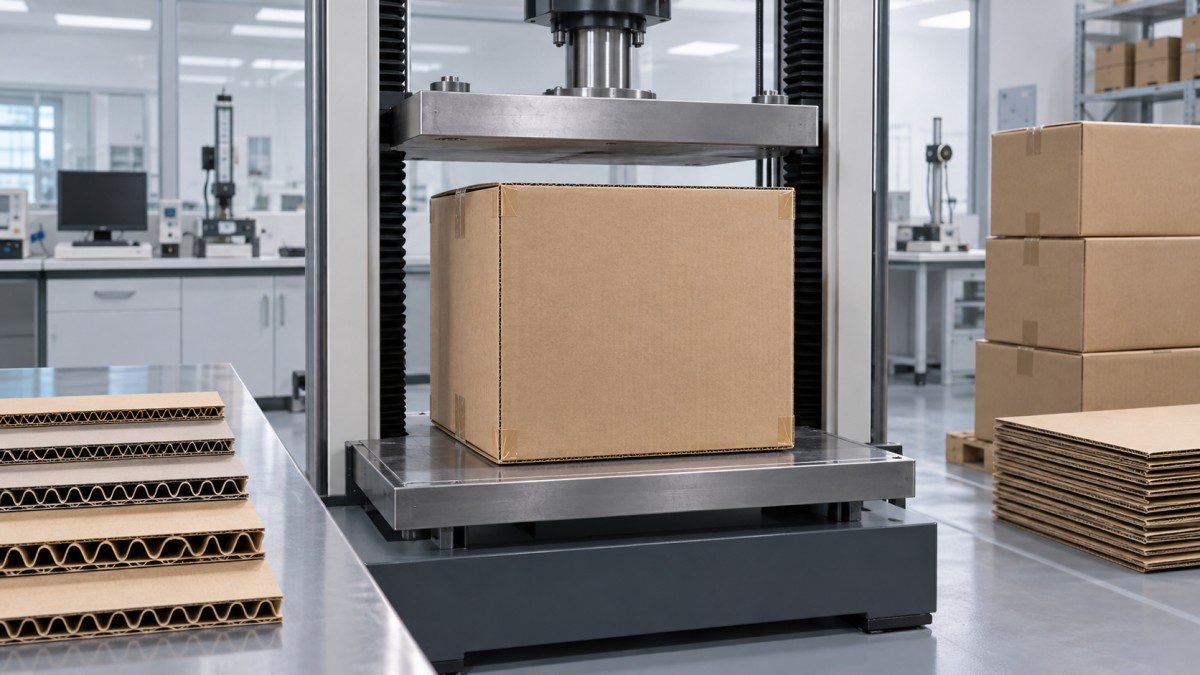
Box compression is frequently the central concern for transit cases, but the result should be interpreted as a system property. Box height, perimeter, score placement, closure design, ventilation openings, load sharing, and time under compression all matter. A laboratory compression value is useful for comparison and quality control; it is not a substitute for understanding the palletized load path.
Edgewise strength is valuable because vertical box walls carry stack loads through their edges. Yet a high edgewise value does not guarantee a high-performing box when the converted blank has weak scores, crushed flutes near folds, poor glue joints, or large cutouts. Flat crush resistance is especially relevant where flutes may be compressed during handling or where a board must retain a consistent surface, but it does not directly answer a stacking question. Matching the test to the expected failure mechanism avoids both under-specification and unnecessary upgrades.
Flute selection changes more than thickness
Flute profile affects cushioning, caliper, print surface behavior, bending stiffness, score response, and material efficiency. A larger flute can provide useful separation and shock absorption, while a finer flute may offer a smoother surface and tighter fold behavior. Combining flute structures can improve performance in demanding cases, but it also changes converting requirements, storage volume, and cost.
Choosing a thicker board simply because the product is fragile is a common shortcut. Fragility is often a product-to-box clearance problem before it is a board problem. If a heavy item is loose inside a larger carton, it can build momentum and overload one panel or corner. Better fit, partitions, pads, or a redesigned load orientation may reduce damage more effectively than adding paper to every wall.
The opposite mistake occurs when a packaging design is optimized only for cube efficiency. Reducing void space can lower freight cost, but too little clearance can transfer impact directly into the product. The appropriate flute and internal protection arrangement depend on the product’s sensitivity, mass distribution, and allowable movement. Corrugated board should be selected as part of that protective system.
Conversion quality often explains failures blamed on board grade
When cases collapse inconsistently, investigation should move beyond the board certificate. Check the blank and the erected box. Are scores straight and correctly positioned? Are flutes excessively crushed at folds? Are slots, hand holes, or cutouts placed near high-load areas? Is the manufacturer’s joint fully bonded and aligned? Does the case erect squarely, or does it lean before it enters the load?
These questions matter because corrugated packaging is designed to carry forces through a three-dimensional shape. A small loss of geometry can redirect load away from vertical edges and into panels that buckle more easily. Uneven moisture, warped blanks, inconsistent score depth, or misapplied adhesive can make performance variable even when the nominal board construction remains unchanged.
For operations using automated die-cutting, folding, and gluing, conversion analysis should include repeatability. A design that works during a short approval run may create waste or jams at production speed if folding force, glue application, or blank registration is unstable. This is where equipment and material evaluation meet: board properties influence machine settings, while machine setup can alter the usable strength of the finished pack.
PWFS tracks the equipment side of this relationship across corrugated board lines and high-speed converting systems. For a technical evaluation, the useful principle is straightforward: evaluate board quality at the point of use, after corrugation and conversion, rather than assuming that raw-paper selection alone defines finished-box performance.
Total cost is driven by failure risk and process fit, not purchase price alone
A lower board price can be expensive when it causes higher damage claims, more packing rejects, poor pallet stability, or additional internal protection. A premium construction can be equally inefficient when it delivers strength the distribution system never uses. The target is the lowest total cost at an acceptable, repeatable protection level.
Build the cost view around the complete packaging system:
- Material consumption: board area, caliper, trim waste, and the effect of flute choice on blank size and shipping cube.
- Conversion yield: setup waste, die-cut quality, folding and gluing reliability, and the frequency of rejected blanks or cases.
- Packing-line behavior: erection reliability, sealing compatibility, downtime, and labor required to correct poor box formation.
- Distribution performance: pallet stability, product damage, rework, returns, and the consequences of a failed case in transit.
- Inventory and logistics: flat-pack storage volume, replenishment frequency, and freight implications of the finished pack.
Do not compare alternatives only on a per-case price. Compare them on a common functional basis, such as the cost to ship one unit through the defined distribution route with the required protection and process yield. This prevents a heavier board from being rewarded merely for having more material, and prevents a lower-cost board from being selected before its operational losses are visible.
A disciplined evaluation sequence
The most reliable packaging analysis begins with the distribution requirement, then works backward into the board specification. Starting with a familiar grade and trying to justify it afterward tends to preserve legacy cost and performance problems.
- Define the product: mass, dimensions, center of gravity, surface sensitivity, allowable movement, and vulnerable features.
- Map the handling route: unit load configuration, stack height, storage duration, likely moisture exposure, manual handling, conveyor transfers, and parcel versus palletized transport.
- Identify the dominant failure modes: compression, puncture, impact, abrasion, moisture softening, poor closure, or converting instability.
- Specify measurable board and box attributes that address those modes, including tolerances and the condition in which samples are evaluated.
- Review finished cases after conversion, not only unconverted board samples. Inspect scores, joints, dimensions, squareness, and any strength-critical cutouts.
- Compare alternatives by protection, runnability, material yield, and delivered system cost. Retain the evidence so future supplier or machine changes can be assessed against the same baseline.
Conditioning deserves particular attention. Corrugated board responds to its environment. A result obtained from a dry, freshly made sample may not represent a case stored in a humid warehouse or moved through a temperature-changing supply chain. The evaluation condition should resemble the use condition closely enough to expose the risks that matter.
When a board upgrade is justified, and when it is not
An upgrade is justified when analysis shows insufficient protection margin under realistic loads, repeated variability in a strength-critical property, unacceptable damage exposure, or a conversion issue that cannot be corrected through design or process control. In these cases, changing liner quality, flute structure, board configuration, or protective design may be appropriate.
It is not automatically justified when failures originate from loose product fit, weak palletization, unsuitable tape or adhesive, excessive ventilation openings, poor scoring, or handling outside the intended distribution profile. Adding board weight can hide the symptom for a time while raising material and freight cost. Correcting the actual weak link produces a more stable specification.
The final specification should make its assumptions visible: product load, box geometry, environmental exposure, stack requirement, conversion configuration, and acceptance criteria. That turns corrugated packaging from a purchasing description into an engineering control. It also gives technical teams a clearer basis for evaluating supplier substitutions, machinery changes, and cost-reduction proposals without sacrificing the protection the pack was designed to deliver.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
