How to Select Tobacco Box Converting Equipment for High-Speed Carton Production
A tobacco carton line can appear productive during a short factory acceptance run and still become unstable when production shifts to premium metallized board, tight artwork registration, frequent SKU changes, or long uninterrupted runs. The visible symptoms are familiar: scuffed cartons, inconsistent creases, glue strings, rejected packs at the downstream machine, and operators slowing the line to protect quality.
The right tobacco box converting equipment is not the machine with the highest stated speed. It is the machine that maintains dimensional accuracy, crease quality, glue placement, and carton squareness at the speeds required by the actual mix of substrates and designs. Selection should begin with the carton specification and the full production flow, then test whether the die-cutter, folder-gluer, inspection system, and controls can hold that specification under realistic operating conditions.
Start with the cartons that create the most risk
Do not base a selection on the easiest straight-line carton in the portfolio. Tobacco packaging often includes compact blanks, narrow glue flaps, reverse folds, embossing, foil effects, windows, heavy ink coverage, coated board, and designs where a small positional error is immediately visible. A machine that runs standard cartonboard smoothly may behave very differently when handling a short blank with a stiff crease pattern or a surface that is prone to marking.
Before comparing suppliers, group the expected work into practical categories:
- Board grades, calipers, coatings, grain directions, and recycled-content variation.
- Blank sizes, including the smallest and most difficult formats rather than only the average format.
- Carton styles: straight-line, crash-lock, multi-panel, inner frame, sleeve, hinged-lid components, or cartons with special folds.
- Surface treatments such as foil stamping, embossing, varnish, soft-touch coatings, or high-coverage printed areas.
- Daily changeover frequency and the expected batch size for each SKU.
- Downstream requirements, particularly packing-machine infeed tolerances and carton orientation.
This exercise usually changes the evaluation. A line intended for long runs of one design can prioritize sustained mechanical stability and automated delivery. A plant with frequent regional artwork variants may value job memory, fast set-up references, modular tooling, and fewer manual adjustments more heavily than peak speed.
Rated speed is only useful when tied to stable output
Suppliers may quote a maximum mechanical speed, but that figure does not describe saleable-carton output. Technical review should distinguish between machine speed, production speed, and stable production speed. The last is the meaningful number: the rate at which the line can run while meeting agreed tolerances, with normal material variation and without excessive intervention.
Ask the supplier to define the conditions behind each output claim. Was the speed achieved on a simple blank? Was the board preconditioned? Were inspection and ejection active? Was glue application operating at the same pattern complexity expected in production? Were cartons delivered in a form that could be accepted by the next process?
A better evaluation approach is to request trials using representative printed sheets or board samples. Observe not just the first acceptable cartons, but stability after the line has reached operating temperature and has run long enough for vibration, glue behavior, and static effects to emerge. Record the reject pattern. Random rejects may point to material inconsistency or handling instability; repeated defects at one location can indicate tooling, transport, or timing issues.
Assess die-cutting and creasing as a system, not as separate specifications
A premium carton may look acceptable immediately after die-cutting but fail later during folding. The root cause is often not the folder-gluer; it can be crease depth, rule selection, board grain, cutting pressure, stripping accuracy, or distortion introduced when the sheet is transported. For this reason, die-cutting capability should be evaluated through the finished carton, not only by inspection of the cut blank.
Focus on repeatability across the sheet and from one sheet to the next. Check cut-to-print registration, nicks, edge cleanliness, stripping of small waste sections, and the integrity of delicate bridges. Examine creases under folding stress. A crease that cracks printed ink, breaks foil, or produces an uneven fold line may create a downstream quality problem even when the die-cut itself appears precise.
Tooling compatibility also deserves attention. The equipment should accommodate the die board format, stripping configuration, counterplate arrangement, and make-ready method required by the anticipated carton range. Faster make-ready is valuable, but only if it does not reduce the ability to tune pressure and crease behavior for demanding substrates. Automated pressure settings can reduce repeated work, yet operators still need controlled access to adjustments when a new material response differs from the stored job.
Folding performance should be judged at the glue seam and the packer infeed
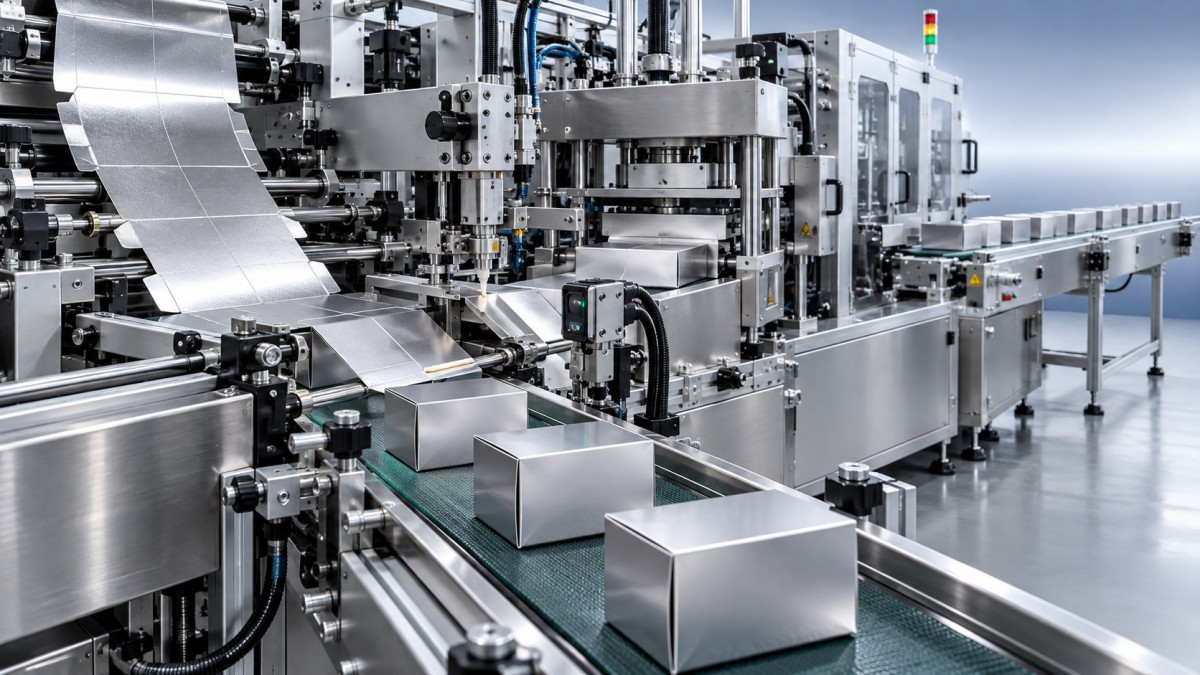
Folder-gluer selection often becomes too focused on belt speed. In tobacco carton production, the more relevant questions concern blank control through each folding section. Short cartons and narrow panels can be sensitive to acceleration, belt pressure, carrier alignment, and fold timing. Any slip between the blank and transport belts can turn a nominally correct set-up into a variable process.
Review the layout of the feeding, pre-folding, folding, gluing, compression, and delivery sections. Confirm whether the required carton styles can be made with the standard configuration or need attachments that add set-up time and mechanical complexity. For cartons with difficult geometry, ask how the system controls panel position before compression and whether it can maintain squareness without excessive belt pressure that marks the printed surface.
Compression length and dwell time matter because adhesive performance is related to both bond formation and carton speed. A line can apply the correct glue pattern yet deliver weak joints if the carton does not receive adequate controlled pressure before it exits. Test the seam after the adhesive has had time to develop its intended bond, rather than judging it only at the machine delivery.
Glue application is a quality-control decision
Choose the gluing method around the adhesive, seam geometry, and verification requirement. Cold glue, hot melt, and other adhesive systems have different open times, viscosity behavior, cleaning needs, and sensitivity to temperature. The equipment should maintain repeatable application across normal speed changes and should allow adjustment without turning every correction into a prolonged stoppage.
For narrow glue flaps, inspect the relationship between nozzle or disc position, blank tracking, and compression. Excess adhesive can squeeze out, contaminate belts, and mark cartons. Insufficient adhesive may create intermittent open seams that are discovered only after packing or transport. Glue-presence monitoring and camera-based inspection can be useful where the cost of an escaped defect is high, but the inspection method must be validated against reflective foil, dark varnish, variable print contrast, and the actual adhesive appearance.
Surface protection and material handling are easy to underestimate
Tobacco cartons frequently carry finishes that make surface contact more critical. A machine may produce accurate folds while creating rub marks, scratches, scuffing, or visible pressure tracks. These defects can originate at feeder belts, guides, transfer wheels, compression devices, collection zones, or even from carton-to-carton contact at delivery.
During trials, inspect samples under the lighting conditions used for routine quality checks. Look at the cartons from multiple angles, especially around foil, dark solids, varnished areas, and embossed features. Ask which contact components are consumable, what material they use, and how quickly they can be replaced. Equipment with adjustable guides and low-mark transport components may be more appropriate than a nominally faster line that requires aggressive contact to retain control.
Static management should also be examined where coated or dry board is involved. Static can affect feeding separation, blank alignment, dust attraction, and delivery stacking. The right response is not automatically to add a static eliminator; first establish whether humidity control, board conditioning, dust extraction, grounding, or feeder settings are contributing to the problem. A supplier should be able to explain how the machine handles these interactions rather than treating them as operator-only issues.
Automation should reduce variation, not simply add screens
Automation has practical value when it removes recurring sources of set-up error. Useful functions may include motorized carriers, programmable belt positions, stored job parameters, automated feeder adjustments, servo-controlled folding elements, and recipe-driven glue settings. Their value depends on how reliably they reproduce a known good condition and how clearly they show when the actual machine state differs from the stored setting.
Examine the operator interface during a realistic format change. Determine whether a job recipe includes all critical settings or only major dimensions. Identify the remaining manual tasks: tooling changes, guides, belts, glue heads, inspection limits, delivery configuration, and safety checks. A claimed rapid changeover should include the time required to complete those tasks, confirm first-off quality, and release production.
Integration with upstream printing and downstream packing should be considered early. The converting line may need to receive production data, report rejects, manage batch identification, or exchange status signals with connected equipment. Interfaces should be specified in concrete terms: what data is required, who owns the mapping, how faults are reported, and what happens when one system is unavailable. Vague assurances of connectivity often become costly during commissioning.
Build the acceptance test around failure modes
A sound acceptance plan uses measurable, carton-specific criteria. Instead of asking whether the machine “runs well,” define what will be checked: cut-to-print position, folded dimensions, diagonal squareness, crease appearance, glue placement, seam strength, surface condition, reject performance, and delivery quality. Tolerances should come from the carton design, print requirements, and downstream equipment needs rather than from a generic machine brochure.
Include conditions that expose likely weaknesses. Run the smallest blank, a heavily finished design, a board grade near the upper stiffness range, and a job requiring multiple folds. Include a planned speed change and a job change. Observe how quickly the machine returns to stable quality after a stop, because restart behavior affects real production efficiency.
It is also sensible to define the inspection approach before the test. Visual checks alone can miss dimensional drift, while purely automated inspection may not reflect cosmetic expectations. Establish sample frequency, measurement tools, defect classification, and the rule for separating set-up waste from recurring process rejects.
Compare lifecycle demands before approving the purchase
Two machines with similar output can create very different operating burdens. Review accessibility for cleaning, adhesive maintenance, belt replacement, die change support, lubrication, and fault recovery. Restricted access can extend stoppages and encourage incomplete cleaning, particularly around glue systems and areas where paper dust accumulates.
Spare-parts strategy should be discussed in terms of the parts most likely to affect uptime: belts, bearings, sensors, glue components, electronic drives, vacuum elements, and wear surfaces. Ask for a recommended critical-spares list and determine which parts are proprietary. Service documentation should show adjustment references, fault logic, maintenance intervals, and approved procedures for restoring machine geometry after replacement work.
Selection is strongest when the equipment is judged as a controlled converting process rather than a collection of headline specifications. A line that maintains blank control, protects premium surfaces, verifies glue and fold quality, and returns predictably to specification after changeover will usually deliver more usable capacity than one chosen only for its maximum speed.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.