How to Compare Die Cutter Quotations Before Approving a Packaging Line Purchase
How to Compare Die Cutter Quotations Before Approving a Packaging Line Purchase
A die-cutter quotation can look deceptively simple: machine price, stated speed, delivery term, and a few optional modules. Yet two offers with a similar headline price may represent very different production capabilities. One may be a workable entry point for short runs and uncomplicated cartons; another may include the register control, stripping configuration, tooling support, and service coverage needed for a demanding folding-carton operation.
For a procurement team approving an automated packaging line, the question is not merely, “Which die cutter costs less?” The more useful question is, “What does this quotation allow the plant to produce reliably, and what costs have been moved outside the quoted price?” That distinction matters when printed sheets must retain tight visual registration, when pharmaceutical or cosmetic cartons have difficult stripping requirements, or when the die-cutter must feed a folder-gluer running at high throughput.
In packaging equipment reviews, the most expensive surprises usually appear at the boundaries: between press and die cutter, between die cutter and folder-gluer, between the quoted machine and the factory utilities, or between the supplier’s commissioning scope and the buyer’s real production expectations. A disciplined comparison of die cutters quotation packages should expose those boundaries before the purchase order is signed.
Start by making every quotation describe the same job
Do not begin with the supplier’s standard specification sheet. Begin with your own production envelope. It should cover the board grades and thicknesses to be processed, minimum and maximum sheet sizes, typical job mix, printed versus unprinted work, required carton geometries, expected daily changeovers, and the actual downstream process. A machine intended mainly for standard folding cartons should not be judged by the same criteria as one expected to process high-value cosmetic sleeves, intricate internal waste patterns, or large-format corrugated work.
The substrate question is especially easy to underestimate. Cutting force, stripping behavior, feeder stability, and blank delivery all change with board stiffness, coating, moisture condition, print coverage, and sheet flatness. A quotation that says “paperboard compatible” is not enough. Ask the supplier to state the applicable substrate range and clarify whether the proposed configuration is suitable for your actual materials rather than a broad theoretical range.
For plants integrating offset printing, die-cutting, and folding-gluing, sheet quality is part of the die-cutting conversation. Registration marks, varnish, curl, powder, and drying conditions can all influence feeding and registration. This is why PWFS treats printing precision and converting performance as connected production variables rather than separate equipment categories. A beautifully printed sheet that cannot run consistently through the converting section still becomes a costly job.
A practical quotation comparison sheet
Put supplier responses into one buyer-controlled matrix. If a supplier cannot answer an item clearly, record it as “not confirmed,” not as an assumed inclusion. That simple discipline prevents optional equipment from being mistaken for standard scope.
Do not compare rated speed without comparing usable output
Speed claims deserve context. A supplier may quote the mechanical maximum under stable conditions, straightforward layouts, suitable board, and experienced operation. That figure has value, but it should not become the sole basis for line-capacity planning. In real production, output is reduced by job changeovers, feeder adjustments, tool preparation, sheet quality issues, stripping interruptions, rejected blanks, and the pace of downstream packing or folding-gluing.
Ask each supplier to separate maximum rated speed from the expected operating range for the job family you intend to run. Request a description of what the estimate assumes: number of colors already printed, board type, stripping complexity, blanking requirement, and number of changeovers. If those assumptions are not stated, two “high-speed” quotations cannot be meaningfully compared.
Cutting force should be reviewed in the same way. More tonnage is not automatically better; the requirement depends on sheet format, substrate, cutting pattern, crease rules, and stripping load. What matters is whether the machine has adequate force and stable pressure control for the heaviest legitimate job in the plant’s planned mix. A weakly specified press section can show up later as incomplete cuts, uneven creases, excessive tool adjustment, or limits on job acceptance.
Read the automation line by line, not as a marketing label
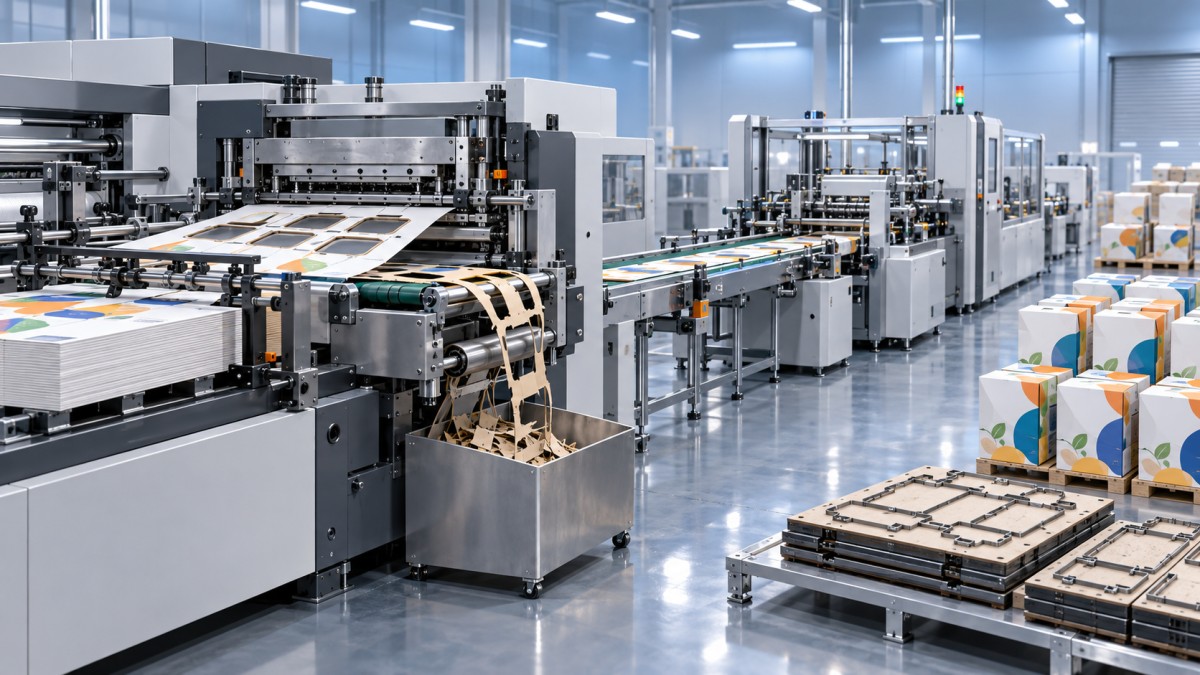
“Automatic die cutter” can describe machines with very different levels of practical automation. One quotation may include non-stop feeding and delivery but leave register correction, pressure adjustment, and stripping setup largely manual. Another may add motorized settings, job recall, camera-assisted inspection, or more advanced waste handling. Neither approach is universally right. The right choice depends on run lengths, operator skill availability, SKU frequency, and the cost of a delayed changeover.
A plant with long, repeatable runs may reasonably favor robust mechanics and straightforward operation over a large automation package. A converter handling many short runs, frequent artwork changes, or premium cartons may place greater value on repeatability and faster setup recovery. Procurement should therefore ask a concrete question: which manual actions are removed, and how are those actions performed on the proposed machine?
Also check the relationship with the folder-gluer. A die cutter that produces blanks faster than the next process can accept them creates pile management and handling pressure. Conversely, a folder-gluer may expose inconsistent crease quality or incomplete stripping that looked manageable at the die cutter. The proposed line should be reviewed as a flow of sheets and blanks, not as a collection of isolated assets.
Treat tooling, installation, and utilities as part of the capital cost
The base machine is often only one layer of expenditure. Some die cutters quotation packages include a limited set of chases or plates; others list them separately. Tooling can also involve stripping frames, blanking equipment, preparation benches, and supplier support for the first production tools. Procurement should distinguish between reusable machine-side accessories and job-specific die tooling, which will remain an ongoing operating cost.
Installation scope requires equally careful reading. Confirm who is responsible for unloading, positioning, foundation preparation, electrical connection, compressed air, extraction where applicable, safety guarding interfaces, and trial materials. International offers may use delivery terms that place transport, insurance, import formalities, or local inland movement outside the supplier’s price. These are normal commercial arrangements, but they must be visible in the total project comparison.
Ask for the machine’s utility requirements in writing and have plant engineering review them before approval. Power supply compatibility, compressed-air quality, floor loading, access routes, and space for maintenance are not details to solve after shipment. A large-format machine may fit on a layout drawing while leaving too little room to change a component, prepare tools, or safely move pallets.
Make acceptance testing commercial, not ceremonial
A quotation should state what proves that the machine has been delivered as promised. Factory acceptance testing and site acceptance testing do not need to be unnecessarily adversarial, but vague language such as “machine runs normally” offers little protection. Better acceptance criteria reflect the buyer’s selected representative jobs, agreed substrates, required functions, safety systems, and the conditions under which the test will be conducted.
Be cautious about accepting a demonstration that uses only a simple sample supplied by the manufacturer. It may show mechanical motion but say little about the more difficult work that justifies the investment. Where practical, submit agreed production samples or a defined test layout early in the negotiation. If the supplier cannot validate a particular complex application before purchase, that limitation should be understood and documented rather than buried in a sales discussion.
Training deserves a similar level of detail. Confirm the number of trainees, training duration, language, shift coverage, included travel arrangements, and whether operators receive instruction on setup, fault diagnosis, preventive maintenance, and safe tool handling. The first months after commissioning are when weak training becomes visible through waste, slow recovery, and dependence on one experienced operator.
Calculate lifecycle exposure before choosing the lowest bid
The best commercial comparison is usually a total-cost view over a defined planning period, not an attempt to predict every future expense with false precision. Include the quoted equipment price, freight and installation items, initial tooling and spares, utilities or facility modifications, operator training, anticipated consumables, maintenance provisions, and the likely cost of downtime support. Some items will remain estimates, but listing them is more honest than ignoring them.
Service capability should be checked at the same time. Ask where technical support is provided from, how remote diagnosis works, which critical parts are recommended for local stock, and what is included during warranty. A supplier with a lower initial price may still be the right choice if its machine is simple, well-supported, and suitable for the workload. Equally, a premium quotation may be justified if its configuration addresses a genuine bottleneck. The decision should follow the production model, not a preference for either low price or maximum specification.
Before approval, issue one final clarification document that lists every inclusion, exclusion, assumption, interface responsibility, and acceptance condition. It is not glamorous work, but it is where procurement protects the packaging line. A comparable die cutters quotation is one that makes the machine, the surrounding process, and the supplier’s obligations equally visible. Once those elements are clear, the capital decision becomes far less about guessing and far more about choosing the operating model the factory can actually sustain.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
