
How Can I Reduce Waste on a Die Cutter?
Waste on a die cutter is rarely caused by one setting alone. It is usually the combined result of inefficient blank layout, unstable sheet position, uneven material behavior, incorrect cutting or creasing pressure, and weak control of make-ready changes. The practical objective is not simply to reduce visible trim. It is to increase the proportion of sheets that become saleable cartons while keeping production speed, print quality, and downstream folding performance under control.
A useful distinction is between planned waste and avoidable waste. Planned waste includes the gripper margin, minimum web or sheet edge requirements, stripping bridges, bleed allowance, and unavoidable skeleton needed to hold blanks together through the machine. Avoidable waste includes oversize trim margins, repeated registration corrections, damaged sheets, cracked scores, incomplete cuts, poor stripping, and cartons rejected after folding or gluing. Reducing the second category usually delivers more reliable savings than trying to remove every millimeter from the first.
Start with a waste map, not a general scrap target
“Waste” should not be recorded as a single production number. A die-cutting job can lose material at several points, and each loss has a different cause and owner. Separate the job into at least these operational categories:
- sheet or board rejected before die-cutting because of print, curl, moisture, or dimensional problems;
- make-ready sheets used for registration, pressure, stripping, and delivery setup;
- structural trim generated by blank layout and die design;
- production rejects caused by cutting, creasing, stripping, or delivery faults;
- downstream rejects found at folding, gluing, packing, or customer inspection.
This separation matters because a layout problem cannot be corrected by increasing operator attention, and a cutting-pressure problem cannot be solved by changing imposition alone. Tracking waste by reason code, job number, material grade, machine, die, and shift creates a more useful picture than recording only total scrap weight. It also prevents a common management error: judging a job as acceptable because the die cutter ran at speed, even though excessive defects were discovered later at the folder-gluer.
For short runs and frequent changeovers, make-ready may be the dominant source of loss. For long, repeat packaging programs, a small improvement in blank utilization or defect rate may matter more because it affects every production sheet. The correction should follow the loss pattern rather than a universal target.
Improve blank layout before changing machine settings
The die layout determines the theoretical yield of the sheet. If the layout leaves large, irregular offcuts or requires unnecessary spacing between blanks, no amount of machine optimization will recover that lost board. Layout review should therefore happen before the die is produced, particularly for cartons with unusual shapes, angled panels, handles, windows, or complex locking features.
Several constraints must be balanced: printed image position, bleed, grain direction, creasing direction, carton strength, stripping geometry, gripper and side-lay requirements, and the minimum bridges needed to retain the blank. A layout that appears highly efficient on screen may prove unstable on the press if stripping tools cannot remove the internal waste cleanly or if narrow bridges break at operating speed.
Sheet rotation can sometimes improve utilization, but it must not be treated as a purely geometric decision. Reversing or rotating a carton can change crease behavior relative to the board grain. It may also affect the direction of printed artwork, barcode placement, varnish scuffing risk, and performance on the folder-gluer. If a carton has a visual front panel, critical embossing, or a directional coating, the additional yield from rotation may not offset the quality risk.
Nested layouts deserve the same caution. Interlocking irregular shapes can reduce skeleton width, but narrow waste channels may be difficult to strip, particularly on lightweight cartonboard, heavily coated stock, or jobs with complex internal cutouts. The relevant question is not “How close can the blanks be placed?” It is “Can this layout run repeatedly without unstable stripping, blank distortion, or excessive stoppages?”
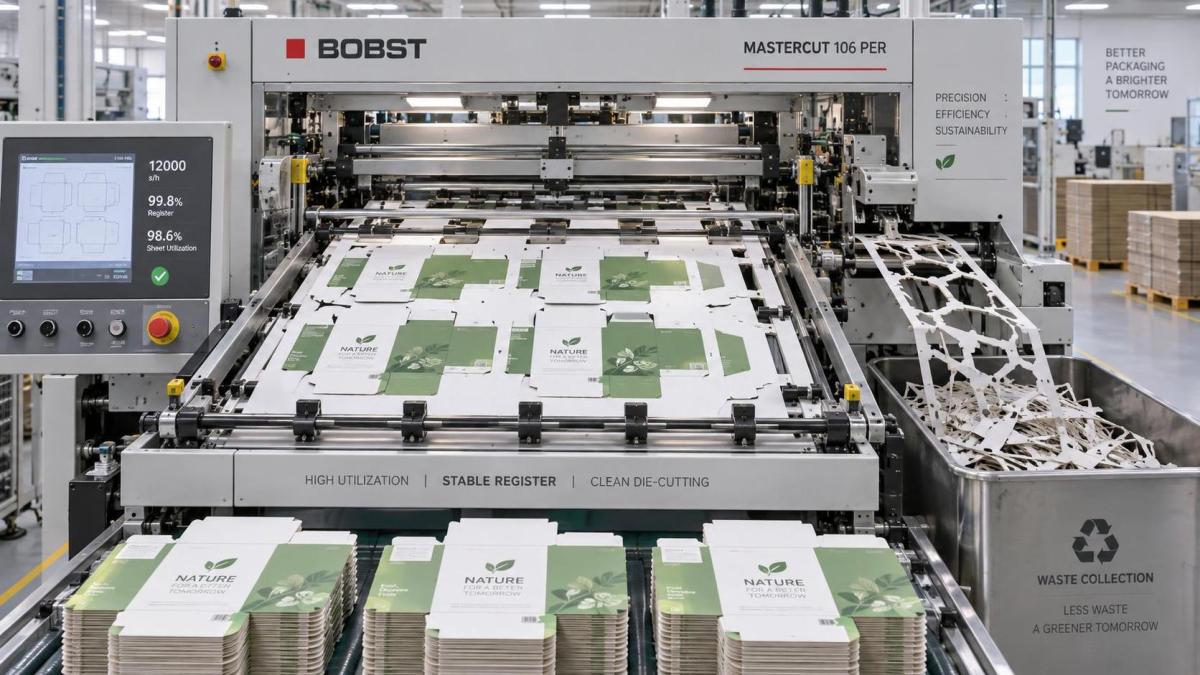
Die designers, prepress teams, and production planners should review the structural drawing together when material cost is high or the carton geometry is demanding. The review should identify where waste is structurally necessary and where it exists only because the layout was inherited from an earlier job or built around an outdated sheet size. Standardizing a small number of efficient parent-sheet formats can also reduce offcut variability, provided those formats remain compatible with printing, warehousing, and customer specifications.
Protect registration before the sheet reaches the cutting station
Misregistration creates waste in two ways. A visibly shifted cut may ruin the carton immediately, but smaller registration movement can also reduce glue flap width, expose unprinted edges, misplace embossed areas, or create unequal borders that fail brand-quality requirements. Die-cutting accuracy depends on stable print-to-cut registration, not on die-cutter settings in isolation.
The inspection point should be the relationship between the printed image and the dieline, especially at narrow borders, windows, reverse folds, and graphics that run close to a cut edge. Registration marks and camera-guided systems can support correction, but they do not compensate for inconsistent sheets, warped stock, inaccurate gripper handling, or unstable printed dimensions.
Printed sheets should be conditioned and stacked so that they enter the feeder consistently. Curl, static, edge damage, loose pile alignment, and variable sheet flatness can create intermittent errors that are difficult to diagnose because the first few sheets may run correctly. Board moisture content and storage conditions are especially important where the stock moves between climates, production sites, or non-conditioned warehouses. Dimensional variation in paperboard can change both cut position and crease response.
When a registration issue appears, avoid correcting it immediately with broad mechanical adjustments. Check whether the deviation is constant, progressive, or random. A constant shift may indicate an incorrect setup reference. A progressive shift can point to feeder or side-lay behavior. Random movement is more likely to involve sheet condition, static, pile quality, or intermittent mechanical wear. Treating all three patterns as the same problem increases make-ready waste and can introduce new faults.
Set cutting and creasing pressure for the material, not for a visual shortcut
Excessive pressure is one of the most expensive false fixes in die-cutting. It may eliminate an incomplete cut temporarily, but it can crush flute profiles, weaken cartonboard, enlarge cut edges, shorten die life, damage the cutting plate, and create score cracks that only become visible during folding. Insufficient pressure, meanwhile, leaves hanging nicks, incomplete cuts, uneven stripping, and poor blank separation.
The correct pressure is the lowest setting that produces a clean cut and functional crease across the full sheet. That condition depends on material caliper, density, coating, moisture, grain direction, print coverage, and die condition. It can also vary within the same nominal board grade. A rigid setup recipe copied from a previous job is useful only when the stock and die configuration are genuinely comparable.
Creasing needs separate attention from cutting. A carton can look acceptable at delivery yet fail when the folder-gluer opens the score at speed. Inspect fold lines for surface cracking, liner fracture, uneven score depth, and fiber rupture. On corrugated work, check whether the crease crushes flutes excessively or creates inconsistent folding resistance. On coated folding carton board, evaluate whether the coating cracks on the outside of the fold.
Make-ready sheets should be used deliberately. Rather than adjusting multiple variables at once, establish a sequence: confirm sheet position, check image-to-die relationship, verify cutting completeness, inspect creases, then test stripping and delivery. When several changes are made simultaneously, the source of improvement or deterioration becomes unclear, and operators may consume more sheets repeating the same troubleshooting cycle.
Keep the die, stripping tools, and cutting surface in matched condition
A die cutter works as a system. A sharp die on a damaged cutting plate may still create inconsistent cuts. A good cutting plate cannot compensate for worn rules, poor ejection rubber, loose stripping components, or a die that has lost dimensional stability. Maintenance should therefore be linked to defect patterns rather than carried out only at fixed calendar intervals.
Signs that tool condition is contributing to waste include incomplete cuts occurring in the same location, waste that fails to release consistently, excessive dust, distorted blanks, recurring hanging nicks, or progressively higher pressure requirements. Raising pressure repeatedly to compensate for declining tool performance usually transfers cost from the die to the board, machine, and downstream process.
Ejection rubber has a direct effect on blank release and sheet stability. If it is compressed, hardened, incorrectly positioned, or uneven in height, the sheet may cling to the die or lift unpredictably. This can cause edge damage, poor stripping, and delivery jams. Stripping pins, upper stripping boards, and blanking tools should also be checked for alignment and wear, particularly after die repairs or long production runs.
Cutting plates require disciplined rotation, inspection, and replacement. Localized damage can produce pressure variation that operators may mistakenly attribute to stock inconsistency. A documented plate history helps distinguish a material issue from a recurring machine-side defect. The same principle applies to chase condition, locking elements, gripper bars, feeder components, and delivery alignment.
Control material variability and job handover
Two pallets marked with the same board specification do not necessarily behave identically in the die cutter. Caliper variation, grain, moisture, coating, stiffness, and print coverage influence cutting and creasing performance. This does not mean that every job requires extensive laboratory testing. It means that receiving checks and production records should identify material characteristics that materially affect setup.
For repeat work, retain a job record that connects board grade, caliper, sheet dimensions, die identification, cutting plate condition, pressure range, registration references, stripping configuration, acceptable defect limits, and downstream observations. A useful record captures the conditions under which the job ran well, not merely the final machine settings. If a repeat run uses a different mill batch, coating, print process, or board storage condition, the prior record should be treated as a starting point rather than a guarantee.
Job handover is another overlooked source of waste. The die-cutting department needs information that prepress, printing, and converting teams may assume is obvious: whether graphics are critical near cut edges, which folds are customer-facing, whether a varnish is brittle, whether glue flaps have tight tolerances, and whether the carton will run on a high-speed folder-gluer or be packed manually. Without this context, a technically “within tolerance” die-cut sheet can still create commercial rejects.
Do not use running speed to hide an unstable process
Higher speed reduces unit processing time only when output remains acceptable. If speed increases sheet skew, stripping failures, delivery jams, cracking, or feeder doubles, the apparent productivity gain can be erased by lost board, extra labor, rework, and delayed delivery. The appropriate operating speed is the highest speed at which critical quality conditions remain stable over a meaningful run, not the highest speed reached briefly after setup.
Monitor the first production segment closely after make-ready, after a pallet change, after tool adjustment, and after any interruption. These transition points often reveal faults before they generate a large volume of scrap. Sampling should include more than visual cutting quality. Check blank dimensions, crease performance, stripping cleanliness, carton squareness, and the condition of samples after folding.
A simple but disciplined escalation rule is valuable: stop and investigate when a defect repeats in the same location or follows a recognizable pattern. Continuing in the hope that a defect will disappear consumes material and makes root-cause analysis harder. Conversely, stopping for every isolated cosmetic mark can create unnecessary downtime. The distinction depends on whether the issue is random, recurring, or systematically linked to a machine position, die feature, or material condition.
Measure the cost that matters
Waste reduction should be assessed in usable output, not only kilograms of scrap. A layout change that saves board but causes slow stripping may not improve job economics. A faster setup that leads to fold cracking may only move rejection downstream. The most meaningful measures connect input sheets to accepted finished cartons and show where losses occur.
For each job, compare planned yield with actual accepted yield, then investigate the gap. Include make-ready sheets, running rejects, trim, rework, and downstream rejection where traceability allows. Material price, print value, coating or foil content, and disposal route can be added to determine which defects deserve the fastest attention. Premium printed board lost after several value-added processes is more costly than unprinted trim, even if both weigh the same.
The durable answer to “How can I reduce waste on a die cutter?” is therefore a controlled workflow rather than a single adjustment: design blanks that can be cut and stripped reliably, stabilize print-to-cut registration, match pressure to the actual stock, maintain the complete tooling system, and use defect data to correct the point where loss begins. That approach reduces scrap without sacrificing the carton quality and process stability on which profitable converting depends.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
