What Does Panel Furniture Production Equipment Cost? A Buyer’s Budgeting Guide
The cost of panel furniture production equipment is best treated as a line-design decision rather than a machine-price exercise. A low-priced CNC router can be the right purchase for a workshop with stable, simple cabinet parts; it can also become an expensive bottleneck when the business depends on nested production, frequent design changes, rapid order release, and consistent drilling accuracy. The same applies to edge banders, drilling centers, loading systems, and software.
For budgeting purposes, a basic semi-automatic panel-processing cell may require a capital allowance in the low six figures in US dollars, while a connected line with automatic handling, return conveyors, labeling, nesting, drilling, and advanced edgebanding can move into the high six figures or beyond. Those broad bands are not quotations. They are planning anchors. The final panel furniture production equipment price depends on what is included at the factory gate, what is required to make the equipment productive on site, and what level of production risk the buyer is trying to remove.
Machine price is only one layer of the investment
Supplier offers often look comparable because they list the same broad machine category: CNC nesting router, automatic edge bander, six-sided drilling center, or panel saw. Yet the quoted values may cover very different scopes. One offer may include installation, software configuration, tooling, and commissioning support; another may cover the base machine only. Comparing the headline figure without normalizing the scope is one of the fastest ways to under-budget a project.
A practical budget separates the investment into five cost layers:
- Core equipment: the machine frame, spindles, saw units, glue system, drills, control, safety guarding, and standard electrical package.
- Production-enabling options: automatic loading and unloading, label printing, barcode scanning, return conveyors, extra tool changers, aggregate heads, PUR glue units, pre-milling, scraping, cleaning, and workpiece tracking.
- Engineering and digital integration: CAD/CAM interfaces, nesting software, production scheduling, ERP or MES connections, post-processors, data preparation, and database setup.
- Site and utility work: foundations where required, compressed air, electrical distribution, dust extraction, material flow space, fire and safety provisions, and network infrastructure.
- Commissioning and ownership costs: freight, insurance, import duties where applicable, installation labor, training, spare parts, tools, consumables, service travel, and expected maintenance.
A budget that includes only the first layer is not a production budget. It is an equipment purchase budget.
What different equipment categories can do to the budget
The range below is intended for early capital planning in USD. It should not replace supplier quotations, because machine configuration, origin, currency terms, regional service requirements, and installation scope can change the number substantially.
The wide ranges are not a weakness in the estimate; they reflect the fact that “CNC router” or “edge bander” is not a meaningful specification by itself. Two machines with the same nominal working width can serve entirely different production models.
The production model should set the budget ceiling
Equipment capacity should be matched to the order profile, not merely to an annual sales target. A manufacturer producing repeated cabinet carcasses with limited material variation may obtain strong value from optimized cutting and standardized drilling. A business making highly customized wardrobes, kitchens, office systems, or mixed-material furniture needs flexibility in part identification, drilling patterns, edge requirements, and routing operations. The latter may benefit more from reliable data flow and rapid setup than from a machine with the highest stated feed speed.
Three operating questions expose whether an equipment proposal fits the production model:
- How many unique parts must be processed in a normal day, and how often do designs change after order release?
- Which operation currently creates the longest queue: cutting, edge banding, drilling, sorting, assembly preparation, or rework?
- Can the proposed machine run productively with the available labor, panel storage method, dust extraction capacity, and software data quality?
A line is constrained by its slowest dependable operation, not by the fastest machine in the quotation. Installing a high-output nesting cell before resolving edge-banding capacity can simply transfer the queue downstream. Likewise, a sophisticated drilling center may not deliver its expected output if panels arrive without consistent labels, correct orientation data, or stable edge reference conditions.
Automation has a cost curve, not a simple yes-or-no value
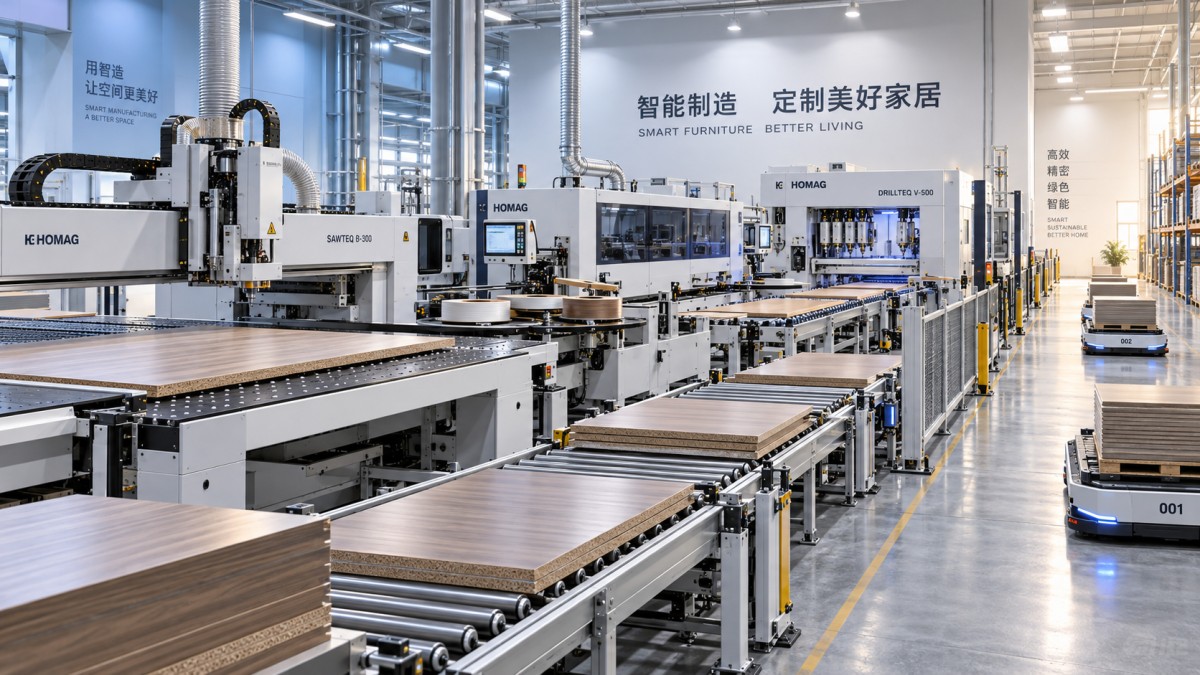
Automatic loading, unloading, return conveyors, robotic handling, labeling, and barcode verification increase the initial investment. Their value is not limited to labor reduction. They can reduce handling damage, stabilize part identification, shorten waiting time between operations, and make output less dependent on individual operator routines. But automation also requires disciplined material flow. A loading system cannot compensate for mixed panel stacks, inconsistent board dimensions, poor label data, or inadequate space around the machine.
The most common budgeting mistake is to treat automation as an optional accessory added late in the discussion. In reality, it affects layout, electrical demand, safety zoning, dust extraction design, software interfaces, installation time, and operator workflows. Retrofitting a return conveyor or automatic loading system may be technically possible, but it can be more disruptive and costly than allowing for it in the initial layout.
That does not mean every facility should purchase a fully automated line. A staged approach can be more defensible where product mix is still evolving. The key is to select machines with credible expansion paths and reserve floor space, utility capacity, and data architecture for the next step. “Upgradeable” should be verified in writing: identify the modules, interfaces, lead times, installation requirements, and whether the original control system can support them.
Edge banding can distort the budget if specifications remain vague
Edge banders are frequently under-specified because buyers focus on panel width and feed speed rather than finished edge quality. Yet the price difference between configurations is often driven by the finishing chain: pre-milling, glue application, pressure zone, end trimming, rough trimming, fine trimming, corner rounding, scraping, and cleaning. Adhesive technology also matters. EVA systems may suit many standard applications, while PUR can improve resistance to moisture and heat in certain use cases, but it introduces different adhesive handling, cleaning, storage, and operating requirements.
Premium visual requirements, narrow workpieces, thick edge materials, shaped parts, frequent color changes, and high-gloss or delicate surfaces all affect the necessary configuration. A lower-cost machine that cannot consistently meet the accepted edge standard creates costs outside the machine: manual touch-up, rework, rejected panels, delayed assembly, and customer complaints. The relevant question is not whether the edge bander can apply tape; it is whether it can produce the required finish across the expected board types and part geometries.
Software, tooling, and extraction are not peripheral expenses
For custom panel furniture, software determines whether design intent becomes usable machine data without repeated manual intervention. The purchase scope should distinguish between design software, CAM or nesting software, machine-control licenses, post-processors, label generation, optimization modules, and interfaces to order-management or ERP systems. A supplier may demonstrate a smooth workflow using sample files, while the buyer’s own library, hardware connectors, drilling rules, and naming conventions require additional configuration.
Tooling deserves the same attention. CNC productivity depends on the correct router bits, drills, collets, aggregates, and tool-management rules. Tool life varies with panel composition, coating, feed rate, chip load, dust removal, and machining strategy. An initial tool package may be sufficient for commissioning but not for sustained production. Include working spares and clarify whether recommended tooling is proprietary, locally available, or dependent on a single supplier.
Dust extraction is another cost that cannot be treated as a generic facility item. CNC routing, sawing, and edge trimming generate different waste streams and airflow demands. Poor extraction affects cut quality, tool life, fire risk management, cleaning labor, and machine reliability. The machine supplier should provide extraction connection requirements and expected air volume data; the extraction provider should confirm performance for the complete connected load rather than one machine in isolation.
Commercial terms can make a low quotation expensive
A disciplined comparison converts every offer to the same commercial basis. If one supplier quotes EXW and another quotes DDP, the numbers are not comparable. Freight, packing, inland transport, insurance, customs formalities, duties, local taxes, unloading equipment, installation labor, travel costs, and commissioning days should be assigned to a single cost sheet.
The same applies to warranty. The useful question is not simply “How long is the warranty?” It is which components are covered, whether travel and labor are included, how remote diagnostics work, where spare parts are stocked, and what response commitment exists after commissioning. A machine with inexpensive replacement parts is not automatically low-risk if delivery takes weeks and the line has no bypass route.
Acceptance criteria should be defined before purchase order release. They may include material types, panel dimensions, machining operations, edge quality expectations, output assumptions, software data exchange, safety functions, and the conditions under which factory acceptance testing and site acceptance testing occur. A stated throughput figure has little value unless the panel mix, loading method, tool condition, operator involvement, and calculation basis are clear.
Build the budget around a landed, operating-ready number
A useful internal approval figure is the landed and operating-ready cost: equipment price plus all expenses required to process saleable panels in the intended facility. It should include a contingency appropriate to the uncertainty of the layout, utilities, software integration, and import process. Contingency is not a substitute for specification discipline; it is protection against the items that remain genuinely unresolved.
The investment case should then be tested against the bottleneck it removes. If the objective is shorter lead time, measure the operations that create waiting and rework. If the objective is lower labor dependence, identify every manual handling point rather than assuming a single automated machine resolves the issue. If the objective is quality consistency, define the defect types that the new equipment is expected to reduce. This prevents a project from being justified by nominal capacity that cannot be converted into finished furniture output.
The most defensible panel furniture production equipment price is therefore not the lowest machine quote. It is the cost of a configuration that fits the product mix, can be installed without unplanned infrastructure gaps, has support and parts coverage proportionate to downtime risk, and produces a verifiable result under the buyer’s own materials and operating conditions.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
