Achieving Micron-Level Color Registration on Multi-Color Sheet-Fed Offset Presses
Micron-level color registration for offset printing is not established by one adjustment, one camera, or a single specification in a press brochure. It is the combined result of sheet transport stability, plate-cylinder geometry, ink-water control, optical measurement, and a closed-loop correction system that remains effective while production conditions change. A press may show excellent registration on a short demonstration run, then drift when paper temperature, stock moisture, speed, or blanket condition changes.
For multi-color sheet-fed offset presses used in premium folding cartons, pharmaceutical packaging, cosmetics, tobacco, and other detail-sensitive work, the useful question is not simply, “Can the press register?” Every modern multi-color press can. The more meaningful question is: can it hold repeatable register across the full run, at normal production speed, on the actual substrates and image conditions the plant intends to print?
That distinction changes how press precision should be assessed. A low registration error reported under controlled conditions is encouraging, but it does not by itself prove stable production capability. The press, consumables, workflow, and operator controls must function as one system.
What micron-level registration means on a sheet-fed press
Color registration describes the positional relationship between successive color separations. In CMYK printing, each unit lays down its image on a sheet that has already passed through previous units. If cyan, magenta, yellow, and black do not land in the intended relationship, fine text gains colored edges, reverse type becomes weak, line art looks soft, and screened images can show visible color shift or moire-like artifacts.
Registration has more than one direction. Circumferential register is the position in the direction of sheet travel. Lateral register is the position across the sheet. Diagonal or skew error occurs when the sheet is not square to the printing units or when one side advances differently from the other. On larger sheets, a small angular error can become a significant positional difference between operator side and drive side.
The word “micron-level” should be interpreted carefully. It describes the scale at which a press must detect and correct movement, not a promise that every point on every sheet will remain at one fixed microscopic value. Registration tolerances must be linked to the job: screen ruling, image content, trapping strategy, substrate stability, brand requirements, and whether the work contains fine reverses, metallic effects, opaque white, or additional spot colors.
A practical acceptance target should therefore be defined as a repeatability requirement over a meaningful run, rather than as an isolated best reading. The target should state the measuring method, register mark design, sheet sampling interval, production speed range, substrate, conditioning state, and allowable variation in both directions.
The mechanical conditions that determine whether correction can work
Automation corrects error; it cannot fully compensate for unstable sheet handling. The feed and transfer path establish the physical reference for every color unit. If sheets arrive at the front lays or side guide with inconsistent position, later corrections become reactive and may create an unstable correction cycle.
Sheet feeder performance deserves close attention. A reliable feeder separates sheets consistently, controls air volume appropriately, and delivers each sheet to the registration system without bounce, skew, or premature contact. Thin coated stock, lightweight paper, static-prone synthetic materials, and warped board each create different feeding risks. A press demonstrated only on flat, well-conditioned paper does not reveal its behavior on more difficult production materials.
Gripper systems are equally important. A sheet can be registered correctly at the feeder and still lose positional consistency if grippers do not hold it uniformly through the transfer cylinders and impression nips. Gripper wear, incorrect pressure, contamination, damaged sheet edges, or variation in gripper timing can cause intermittent register faults that appear random in printed samples.
Cylinder construction, bearer condition, gear or gearless drive accuracy, and unit-to-unit mechanical alignment establish the foundation for repeatable image placement. On conventional mechanically linked presses, backlash, wear, and bearing condition can gradually influence register behavior. On electronically synchronized systems, servo control and encoder feedback add flexibility, but they do not eliminate the need for rigid mechanical structure. A precise digital command cannot correct cylinder vibration, poor sheet hold, or excessive blanket deformation.
Blankets and packing are often treated as maintenance details, although they directly affect image transfer and can influence perceived register. Uneven blanket compression, incorrect packing, localized damage, or inconsistent plate mounting can make a color appear to move even when the sheet is transported correctly. Before attributing a defect to automation, the press team should rule out unit-specific plate and blanket issues.
Optical register systems: valuable only when their reference is reliable
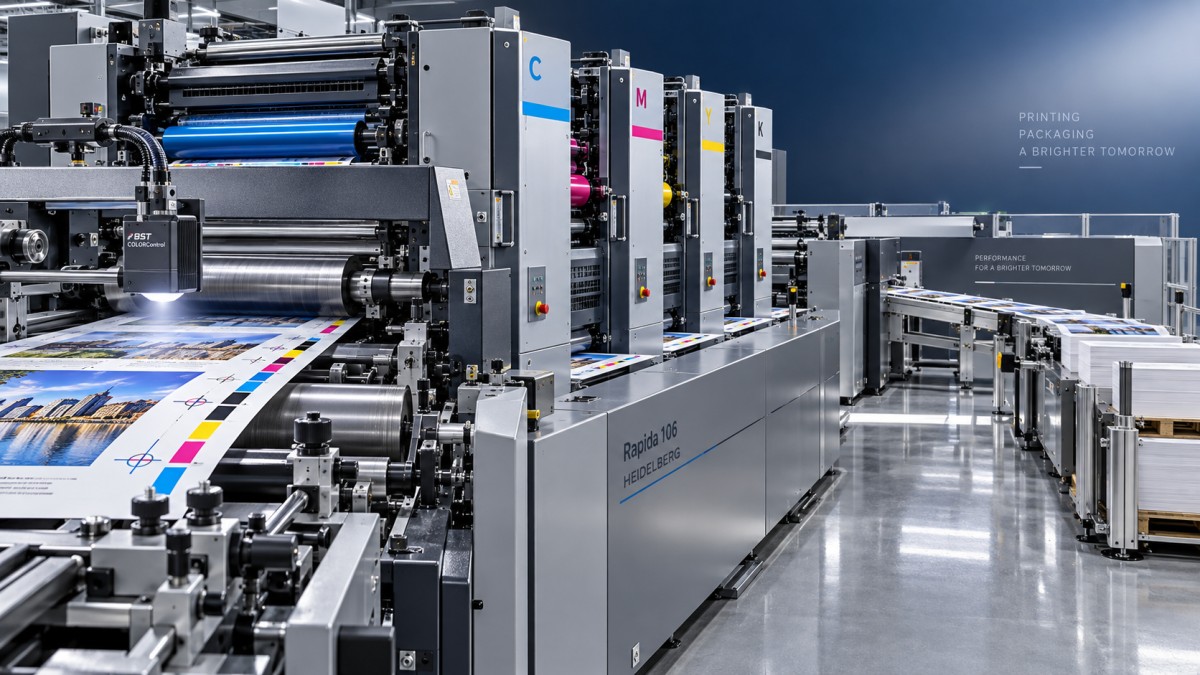
Modern sheet-fed presses commonly use cameras or scanning sensors to read register marks and feed positional error back to the control system. This is a major advantage in frequent-change packaging production, particularly where multiple spot colors, opaque inks, varnish, or reverse-side printing increase setup complexity. Yet an optical system is only as dependable as the marks it reads and the conditions under which it reads them.
Register marks need adequate contrast, clear geometry, and a stable location outside the finished design. Marks placed too close to a trim edge, a heavy solid, a coating boundary, or a contaminated area may deliver inconsistent readings. A mark that is easy to inspect visually is not always ideal for automated measurement. The press supplier should demonstrate how the system handles the mark conventions used by the plant’s prepress workflow.
Substrate surface and ink sequence also matter. Reflective metallic stocks, highly absorbent boards, transparent films, strongly textured papers, and heavy opaque inks can complicate optical detection. The issue is not that these jobs cannot be controlled; it is that their inspection logic, mark design, and acceptable correction response may need to differ from standard coated-paper work.
Evaluate whether the system measures every sheet, selected sheets, or samples at intervals. Continuous inspection can identify rapid movement, but it may be unnecessary for every application. Periodic measurement may be sufficient for stable, long-run work, provided the press has dependable sheet transport and the sampling rule catches drift before waste becomes material. More sensors do not automatically mean better production control if their readings cannot be acted on consistently.
Closed-loop control must distinguish drift from noise
The control loop receives a measured deviation, determines whether it is meaningful, and applies a correction through the relevant printing unit or sheet control mechanism. The difficult part is not calculating a correction. It is deciding when not to correct.
If the system reacts aggressively to normal measurement noise, it can chase variation and create oscillation: one correction moves the register too far, the next attempts to reverse it, and production becomes less stable. If correction thresholds are too loose, genuine drift continues until it is visible in the printed product. A capable configuration uses sensible tolerance bands, correction limits, and filtering that reflect the press speed, job sensitivity, and substrate behavior.
Automatic register control should also be assessed at startup, during acceleration, after wash-up, following a plate change, and during normal steady running. These are different operating states. A press may recover quickly from a controlled stop yet take longer to stabilize after major environmental or ink-balance changes. The recovery profile matters because it determines how much material is consumed before approved sheets are produced again.
Integration with presetting data is another practical factor. Plate imaging data, CIP-style ink-key presets, job parameters, register targets, and stored production recipes can shorten the path to stable color. However, stored settings should be treated as a starting point. Paper batch variation, plate condition, fountain solution balance, and machine maintenance state still affect the run.
Registration is inseparable from sheet condition and pressroom control
A technically capable press cannot force an unstable sheet to behave like a stable one. Paper and board respond to moisture and temperature. Their dimensions can change, curl can develop, and local stresses can appear as sheets pass through drying, coating, or multiple printing units. These changes may present as lateral movement, fan-out, or diagonal register variation.
Fan-out deserves particular attention on multi-color work. As a sheet accepts ink and fountain solution, its dimensions may change across the run. The result may be good register near the gripper edge but increasing error farther through the sheet. This cannot always be solved by a simple circumferential adjustment. It may require compensation functions, revised ink-water settings, different stock conditioning, or a job-specific tolerance strategy.
Ink-water balance affects more than color density. Excessive water can contribute to paper distortion and unstable trapping, while excessive ink can alter dot gain and make a registration problem appear worse than it is. The objective is not merely to maintain a visible image; it is to maintain a controlled print condition in which the sheet remains dimensionally manageable and the optical system reads marks consistently.
For carton work that proceeds to die-cutting and folder-gluing, press register should not be evaluated in isolation. The printed image may be within its internal tolerance yet still be poorly aligned with later cutting, creasing, embossing, foil stamping, or window patching. Job control marks and process references should support the entire converting chain. PWFS tracks this connection between high-precision offset printing and downstream packaging geometry because a visually accurate sheet is only valuable when it converts accurately as well.
A useful press evaluation protocol
The most informative assessment is a structured production trial, not a showroom print. Use representative artwork with fine type, reverses, screened images, solids, and any special colors that are normal for the intended product mix. Include the actual stock grades where possible, especially materials known to curl, stretch, or challenge feeding.
- Define the register standard before the trial. State the permitted deviation, directions to be measured, register-mark format, measurement instrument, sampling method, and pass/fail rule.
- Run through normal operating conditions. Assess startup, speed changes, steady production, and recovery after an interruption. A stable first stack is not enough evidence.
- Measure across the sheet and through the run. Check both sides of the sheet and inspect the sequence of samples rather than averaging away intermittent faults.
- Record correction behavior. Note how often corrections occur, their magnitude, whether the system settles smoothly, and how quickly acceptable production resumes after a disturbance.
- Separate print register from visual color issues. Confirm plate mounting, blankets, ink density, trapping, and dot gain before assigning every defect to register control.
- Test operator workflow. Determine whether setup, mark selection, alarm handling, and job recall can be completed reliably without requiring exceptional operator intervention.
The trial should also reveal what data can be retained. Trend charts, alarm history, job recipes, and inspection records are useful when they help maintenance teams distinguish a repeatable mechanical issue from a substrate-specific event. Data without clear operating decisions attached to it adds little value.
Common evaluation mistakes
The first mistake is accepting a single maximum-speed claim as proof of production precision. High speed is relevant, but registration quality should be judged at the speeds the plant will actually use for demanding work, with realistic drying, coating, and delivery conditions.
The second is treating automatic register as a substitute for preventive maintenance. Cameras and servo adjustments can reduce intervention, but worn grippers, damaged cylinder surfaces, poor plate mounting discipline, or contaminated sensors will eventually defeat the control loop.
The third is specifying a tolerance without specifying the job. Fine black type reversed from a saturated background may require much tighter visual control than a large-format image with generous trapping. A universal number can either over-specify ordinary work or under-protect critical packaging.
The fourth is ignoring downstream alignment. If die-cut, crease, foil, and print references are managed separately, the plant may meet press-side color targets while still generating rejected cartons. Registration strategy needs a common physical reference from prepress through converting.
What should be confirmed before selecting or upgrading a press
Prioritize evidence of repeatability over headline precision. Confirm how the press registers difficult substrates, how sensors perform with the expected ink and coating combinations, which corrections are automatic, and where operator judgment remains necessary. Ask for the maintenance points that most affect registration stability and the diagnostic information available when the system cannot hold target.
Also examine the workflow around the press. Stable plates, disciplined blanket and packing practices, conditioned substrates, consistent register marks, and clear approval criteria are not secondary requirements. They are part of the same precision system.
The strongest multi-color sheet-fed offset setup is therefore not the one with the most impressive isolated specification. It is the one that keeps sheet position, image transfer, measurement, and correction under control across the real mix of jobs the plant must deliver.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.