Packaging Equipment Selection Criteria for Throughput, Changeovers, and Total Cost
Packaging Equipment Selection Criteria for Throughput, Changeovers, and Total Cost
Selecting packaging machinery is a capital decision that shapes much more than the output of one process. It influences plant capacity, labor allocation, waste levels, delivery reliability, maintenance exposure, and the practical range of packaging formats a business can support. For technical evaluators, the challenge is rarely finding a machine with an impressive headline specification. The harder task is determining whether that machine will sustain the required performance with the actual materials, artwork, operators, job mix, and downstream constraints found on the production floor.
The most useful packaging equipment selection criteria therefore begin with a simple distinction: nameplate speed is not productive capacity. A die-cutter, folder gluer, printing press, cartoner, or corrugated converting line may be mechanically capable of a stated maximum rate, yet real output is shaped by setup losses, sheet or board variation, inspection holds, micro-stoppages, quality rejects, and the pace of upstream and downstream equipment. A sound investment review treats the machine as part of a production system rather than an isolated asset.
This systems view is especially important in packaging plants serving short promotional runs, e-commerce fulfillment, regulated consumer goods, or brands with frequent artwork revisions. The same principle applies across industrial paper and wood processing: a highly capable machine only creates value when material flow, digital data, operators, maintenance practices, and quality requirements are aligned around it.
Start with the Production Profile, Not the Machine Category
Before comparing suppliers, define the work the equipment must perform over a normal operating period. “We need more speed” is not yet a technical requirement. Evaluators should establish the expected order mix, annual volume, peak demand periods, board or substrate range, format sizes, print coverage, structural complexity, acceptable defect rate, and required traceability. The profile should also identify what changes most often: carton dimensions, die layouts, ink colors, adhesive patterns, paper grades, flute profiles, or customer-specific labeling data.
For example, a high-volume corrugated operation running a limited set of standard shipping cases will judge equipment differently from a folding-carton converter handling many cosmetic, pharmaceutical, or seasonal SKUs. The first may prioritize stable web handling, heat and steam control, board quality consistency, and uninterrupted material supply. The second may place more weight on registration stability, die-cutting precision, glue control, inspection, and repeatable rapid changeovers. Neither priority set is inherently better; it reflects the economics of the job mix.
The same discipline matters when packaging equipment interfaces with furniture or panel-production workflows. CNC routers and edge banders can support customized display fixtures, retail packaging components, or integrated living-space projects, but their output is governed by CAD/CAM data quality, nesting logic, tool condition, dust extraction, and panel handling. Buying isolated speed without mapping the whole process often transfers the bottleneck rather than removing it.
Measure Throughput as Good Output per Scheduled Hour
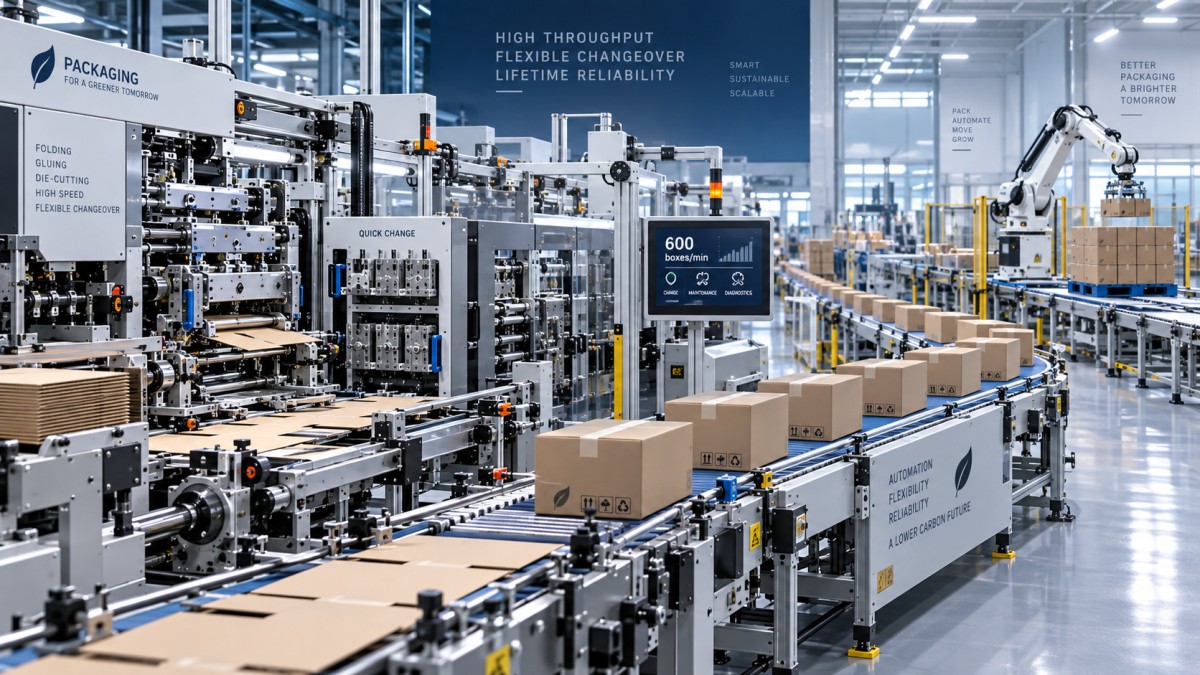
A practical throughput model starts with sellable output, not cycles per minute or sheets per hour. Ask suppliers to clarify the conditions behind every claimed rate: material specification, format, blank design, print coverage, number of colors, adhesive type, inspection configuration, operator involvement, and whether the demonstration run includes production-grade quality checks. A machine can run quickly under simplified test conditions while performing very differently on coated stocks, lightweight corrugated board, heavily printed work, complex lock-bottom cartons, or material with normal batch variation.
Technical teams should review the complete line balance. If a fast folder gluer feeds a packing station that cannot keep pace, finished-carton accumulation may cause scuffing, compression, or unplanned stops. If an offset press produces sheets faster than the curing, die-cutting, or stripping stage can absorb, work-in-process expands and delivery lead time may not improve. At corrugated plants, board-line performance also depends on paper logistics, conditioning, starch preparation, steam availability, and dry-end stability. The nominal capacity of one machine is not the capacity of the factory.
Request a loss tree during evaluation. It should distinguish planned downtime, job setup, material replenishment, quality adjustment, mechanical stoppages, cleaning, tool or plate changes, and downstream waiting time. The format does not need to be elaborate. Its purpose is to reveal where expected capacity disappears and whether the proposed design addresses the dominant losses. This is often more revealing than an unqualified utilization estimate.
Quality stability is part of throughput
High-speed packaging production is only useful when it preserves specification. In offset printing, registration, color consistency, ink-water balance, drying or curing behavior, and sheet transport all affect usable output. A press that requires repeated correction to keep color within the customer’s approved tolerance can consume the apparent gain from higher running speed. In die-cutting, factors such as cut quality, crease consistency, stripping reliability, and blank delivery affect both productivity and carton performance further down the line.
This is why trials should include representative materials and difficult jobs, not only ideal samples. Technical evaluators should define acceptance observations in advance: registration behavior over a sustained run, waste during startup, consistency after speed changes, defect handling, adhesive placement, and the quality of output after normal stacking or packing. Where food contact, pharmaceutical packaging, or forest-product traceability is relevant, the exact compliance requirements must be checked against applicable market rules, substrate declarations, ink and adhesive documentation, and the customer’s own specifications.
Changeover Performance Is a Commercial Capability
Changeover time is often discussed as an efficiency metric, but it is also a sales and planning issue. A plant that can switch formats, artwork, and tooling predictably can accept a broader range of order patterns without destabilizing its schedule. That flexibility matters when brand owners demand smaller batches, more variants, localized graphics, or shorter replenishment cycles.
Do not accept a single “changeover time” figure without defining the change. Moving between similar carton sizes is not equivalent to changing board grade, print design, die set, glue pattern, or complex structural format. For corrugated equipment, consider changes in paper grade, flute profile, web width, and process settings. For printing presses, distinguish between plate change, wash-up, color adjustment, coating changes, and quality approval. For folder gluers, assess carrier settings, belt arrangements, folding modules, glue systems, collection devices, and operator access.
The best evaluation question is: which tasks are automated, which tasks are guided, and which still depend on individual operator skill? Servo positioning, stored recipes, barcode-driven job recall, quick-release tooling, automated cleaning functions, and visual setup guidance can reduce variability. Yet automation should be judged by its reliability and serviceability. A complicated automatic feature that is difficult to diagnose may not improve availability in a plant without the necessary technical support.
Automation Must Fit the Operating Model
Automation can reduce repetitive handling, improve traceability, and make performance less dependent on scarce manual skills. It can also introduce integration and recovery challenges. The relevant question is not whether the machine has a sophisticated human-machine interface or a long list of sensors. It is whether the equipment can exchange usable information with the plant’s workflow and whether operators can recover safely from routine exceptions.
For packaging converters, useful integration may include job data from MIS or MES systems, production-status reporting, recipe management, inspection records, and maintenance alerts. The data architecture should be reviewed early. Determine who owns the interface scope, how job data is validated, what happens when a connection is lost, and whether historical machine data can be exported in a workable format. A digitally connected line that requires manual re-entry of critical job parameters remains exposed to avoidable errors.
Automation should also be evaluated against labor reality. A highly automated palletizing, feeding, or inspection solution may be justified where repetitive work is difficult to staff and volume is stable. In a highly variable environment, modular automation and clear manual fallback procedures may be more sensible. The decision should reflect the expected production mix over several years, not simply the most demanding job currently on the schedule.
Calculate Total Cost Beyond the Quotation
Total cost of ownership is where technically similar proposals often separate. Purchase price matters, but it is only one component. The full cost picture includes installation, foundation or floor preparation, power and compressed-air demand, steam or thermal requirements where applicable, extraction, safety systems, tooling, spare parts, consumables, commissioning, operator training, preventive maintenance, software licenses, and the likely cost of production interruption.
Energy and materials should be assessed in relation to the product mix. A corrugated board line may require close examination of steam efficiency, heat recovery options, paper handling, starch-system management, and waste at startup. A printing operation should consider ink, coatings, wash-up media, plates, blankets, drying energy, and make-ready sheets. For die-cutting and folder-gluing, die life, stripping components, glue consumption, belt wear, and the accessibility of wear parts may materially affect operating cost.
Maintenance is not a side issue. Review service intervals, lubrication design, diagnostic capability, access points, recommended critical spares, remote-support arrangements, and the availability of qualified technicians in the intended region. Ask for a clearly structured spare-parts recommendation for commissioning and early operation. The aim is not to stock every component; it is to understand which failures would stop production and what recovery time is realistically possible.
Use Factory Acceptance and Site Commissioning as Decision Gates
A well-written technical specification converts assumptions into testable obligations. It should define the materials, formats, quality expectations, safety scope, utility conditions, interfaces, documentation, training, acceptance method, and responsibilities for peripheral equipment. If the project includes a factory acceptance test, the test should use agreed representative work where feasible and record the operating conditions rather than merely demonstrating motion.
Site acceptance deserves equal attention because installation conditions can change machine behavior. Material storage, plant temperature and humidity, air quality, steam stability, electrical supply, operator training, dust extraction, and upstream material preparation all affect outcomes. Commissioning plans should include time for tuning the line, validating product recipes, training multiple shifts, and establishing maintenance routines. Treating this phase as an administrative handover is a common source of delayed ramp-up.
At PWFS, the equipment landscape is viewed through the connected realities of corrugated board production, precision offset printing, die-cutting and folding, and digitally driven wood processing. That perspective is useful because the recurring questions are similar across these disciplines: where does variation enter the process, how does it affect yield, and which mechanical or digital controls make the process repeatable without making it unnecessarily fragile?
A Defensible Equipment Decision
The strongest packaging equipment selection criteria connect capital spending to a defined production reality. They compare good output rather than stated speed, distinguish genuine format flexibility from marketing shorthand, test automation against the operating model, and account for lifecycle cost before the purchase order is issued. They also leave room for practical questions: Can operators run it confidently? Can maintenance teams restore it quickly? Can the line meet customer quality expectations on difficult work, not only on ideal samples?
Before finalizing a decision, technical teams should revisit the highest-risk assumptions with the proposed supplier: representative run conditions, complete changeover definitions, interface responsibilities, utility limits, critical spares, acceptance criteria, and the expected support path after commissioning. That review may feel more demanding than comparing top-line specifications, but it is where capacity plans become credible production plans.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.