Selecting Flexible Packaging Structures for Barrier, Seal Strength, and Pouch Speed
Start with the failure mode, not the film name
Flexible packaging structures should be selected from the product outward. A pouch that holds dry snack pieces, a retortable meal, a powdered chemical, and an oxygen-sensitive coffee product may all look similar on a shelf, yet they impose very different demands on barrier, seals, and converting equipment. Choosing a familiar laminate because it has worked elsewhere can produce a package that passes an initial bench test but fails during filling, distribution, or high-speed pouch production.
For technical evaluators assessing flexible packaging solutions for pouch packaging, the practical question is not which material has the highest barrier or strongest seal in isolation. It is which complete structure maintains the required product protection and package integrity at the intended line speed, through the expected shelf life, with acceptable process variation.
A structure is therefore a system: outer web, printed surface or reverse print, adhesive or extrusion tie layer, barrier layer, sealant layer, and sometimes coatings or functional treatments. A change in any one layer can alter stiffness, heat transfer, seal initiation, curl, coefficient of friction, odor, migration risk, or web handling. The evaluation should begin by identifying what failure is least tolerable: moisture pickup, oxygen ingress, aroma loss, seal leakage, pouch distortion, contamination in the seal area, or unstable output on the pouching line.
Barrier performance has to match the product and the pack format
Barrier selection is often reduced to a discussion of oxygen transmission rate or water vapor transmission rate. Those measurements matter, but they do not fully describe package performance. Barrier needs depend on the product's sensitivity, residual headspace, fill condition, target shelf-life window, storage exposure, and package geometry. A wide stand-up pouch with folds, gussets, and a zipper exposes more potential weak points than a simple three-side-seal sachet.
Products that lose texture when exposed to humidity require control of moisture ingress. Products containing fats, natural colors, or oxidation-sensitive ingredients may require stronger oxygen protection. Aromatic products can need both aroma retention and resistance to external odor pickup. Aggressive contents introduce another question: whether the inner layer maintains its physical and chemical integrity when exposed to oils, acids, alcohols, surfactants, or product particulates.
Metallized films, aluminum foil, coated films, EVOH-containing structures, and high-barrier transparent films all have roles, but their selection should reflect the actual risk rather than a preference for the most protective option. Aluminum foil offers excellent barrier when it remains intact, yet it can be vulnerable to flex cracking and pinholing in demanding handling conditions. Metallized films can provide useful barrier at lower stiffness and material weight, though barrier performance may be affected by folds, abrasion, and lamination quality. Transparent barrier films may be appropriate where product visibility is needed, but their performance must be evaluated in the final laminate and pouch shape.
The final construction matters more than the nominal property of an individual web. Barrier layers can be compromised by repeated flexing near a gusset, tension peaks during converting, zipper insertion, scored tear features, or a poorly controlled adhesive application. A laboratory film value should therefore be treated as a material-screening input, not proof that a finished pouch will meet shelf-life expectations.
Technical teams should also avoid treating barrier as a permanent fixed value. Temperature and humidity exposure can change transmission behavior. High temperature filling, retort processing, or extended warehouse exposure may place a structure under conditions that differ materially from standard laboratory testing. A package intended for ambient dry filling has a much wider material set than one that must tolerate hot filling or thermal processing.
Seal strength is a process window, not a single test result
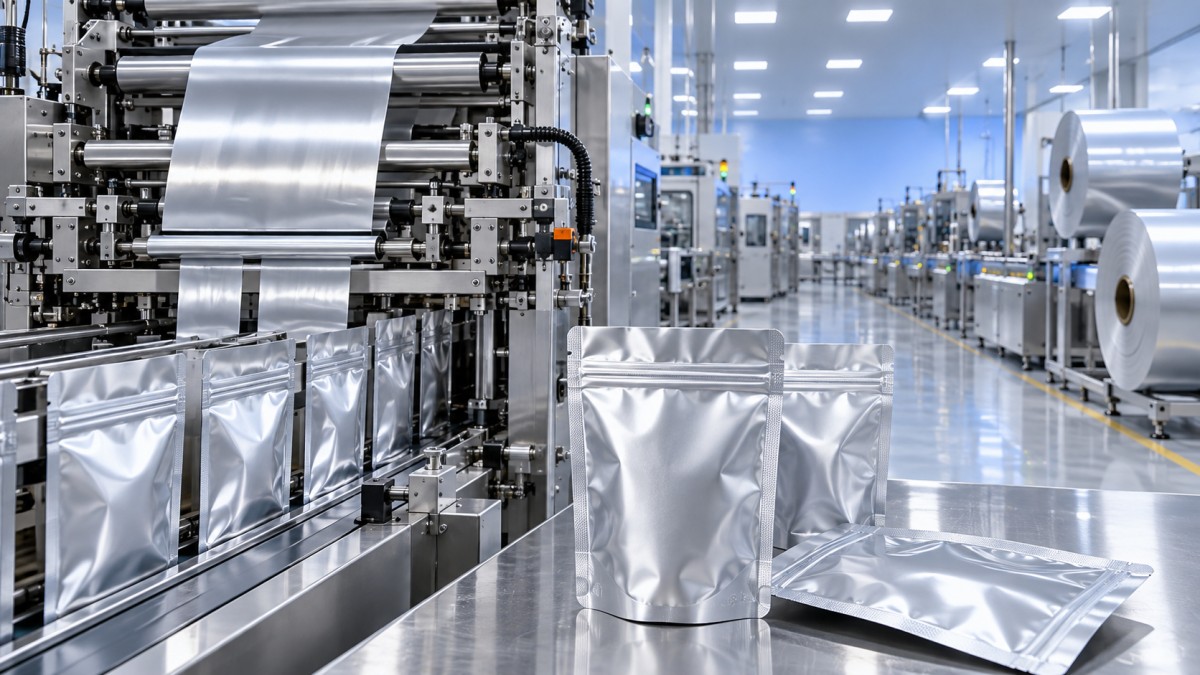
A pouch fails when its seal fails, and seal failure is rarely explained by peel-strength data alone. The sealant must form a reliable bond over a realistic range of temperature, dwell time, pressure, and contamination conditions. It must also tolerate the way the pouch will be handled after sealing: drop impact, compression, flexing, transport vibration, and opening by the end user.
Seal strength should be separated into several related questions:
- At what temperature does the sealant begin to form an acceptable seal?
- How broad is the usable sealing window before distortion, burn-through, sticking, or appearance defects occur?
- Does the seal remain sound when powder, oil, liquid splash, or product particles reach the seal area?
- Will the seal fail by controlled peel, cohesive tearing, film rupture, or adhesive delamination?
- Does the seal retain performance after the intended storage and transport exposures?
A high ultimate seal-strength value can mask a narrow operating window. That is a concern on fast equipment, where small changes in jaw temperature, pressure distribution, web alignment, or dwell time may appear more frequently. Conversely, a sealant designed for lower-temperature sealing can support speed, but it must be compatible with the product, the outer structure, and the desired finished-pouch stiffness.
Contamination tolerance deserves special attention for powders, granules, sauces, and products with irregular particulates. Clean-seal trials can make nearly any suitable sealant look robust. The more relevant question is how the structure behaves under the likely contamination pattern and fill accuracy of the actual machine. A sealant that performs well with a lightly dusted seal area may fail when fine powder is pressed into the interface or when product residues migrate under the sealing jaws.
Seal geometry also changes the requirement. Narrow seals may need higher consistency than wide seals. Spouts, fitments, zippers, and valves introduce interfaces between materials that may require separate validation. For pouches intended to be opened and reclosed, the hermetic primary seal and the reseal feature should be evaluated as separate functions. A convenient zipper does not compensate for a weak bottom seal, and a strong perimeter seal does not prove that the zipper insertion zone is reliable.
Pouch speed changes the material decision
Many structure decisions are made around product protection and then handed to operations to “make run.” That sequence creates avoidable problems. A laminate can be technically adequate at low speed yet generate frequent stoppages, poor registration, seal variation, or tracking problems once output targets rise. Pouching speed is not simply a machine setting; it is a constraint on how much process variability the structure can absorb.
At higher speeds, web tension control becomes less forgiving. Excess curl, uneven caliper, inconsistent slip, inadequate stiffness, poor lay-flat behavior, or variable roll winding can disrupt forming and registration. Films with different thermal responses may move differently through a heat-seal zone, creating distortion or seal misalignment. A laminate that looks flat on a sample table may still cup, telescope, or wander under dynamic tension.
The sealant has a direct relationship with speed because the available dwell time falls as the machine cycle accelerates. If the necessary seal temperature rises to compensate for shorter dwell, the structure may approach a point where the outer web distorts, inks are affected, or the film sticks to the jaws. The most productive construction is often one that provides an adequately wide sealing window at the line’s planned operating range, rather than one optimized for the highest possible seal strength under ideal slow-cycle conditions.
Film gauge should be assessed as part of this operating picture. A thicker layer may improve puncture resistance or stiffness, but it can increase thermal mass and change sealing response. Reducing gauge may lower material use but make registration, handling, puncture resistance, or pouch formation less stable. Gauge reduction is not automatically a cost improvement when it raises scrap rates or requires a lower line speed.
Build the specification around conditions that will actually occur
A useful specification translates product and equipment realities into testable requirements. It should not stop at a generic description such as “high-barrier laminated pouch film” or “food-grade sealing layer.” Those descriptions leave too much interpretation to the converter and make comparison between candidate structures difficult.
The product side of the brief should establish fill temperature, particle size or powder characteristics, oil or acid exposure, headspace gas where relevant, target storage conditions, and the package’s expected abuse profile. The equipment side should define pouch format, sealing method, planned speed range, jaw configuration, cooling conditions, registration requirements, and any features such as zippers, spouts, hang holes, or laser scoring.
It is also useful to identify which variables are fixed and which can be adjusted. If the filling machine cannot provide additional dwell time, the material must meet the speed requirement. If the product formulation is likely to change, chemical resistance and seal compatibility need more margin. If a package will be distributed through channels with poorly controlled temperature or rough handling, a narrowly optimized structure leaves little room for real-world variation.
Samples should be converted into the intended pouch configuration before major decisions are made. Flat-laminate data cannot reveal every issue associated with gusset folds, bottom seals, zipper zones, or forming stresses. The most informative qualification sequence combines material tests with machine-representative trials: runnability at normal and upper planned speeds, seal testing across a realistic process range, leak checks, visual inspection after flexing, and retention testing after relevant conditioning.
Balance simplicity against performance claims
Complex laminates can solve real problems, but each additional layer, coating, or functional feature adds interfaces that must remain stable through conversion and use. More complexity can increase lead-time risk, make troubleshooting harder, and complicate end-of-life pathways. It should be justified by a specific functional need: barrier, puncture resistance, print protection, seal behavior, chemical resistance, or compatibility with a processing condition.
At the same time, simplified structures should not be accepted on the assumption that they will behave like conventional high-performance laminates. A move toward mono-material or reduced-material designs may change stiffness, barrier behavior, heat-seal range, or print protection. The appropriate evaluation question is whether the revised structure satisfies the package’s defined performance envelope, not whether it uses fewer material types.
Comparing candidate structures on unit cost alone can produce misleading decisions. The relevant cost is the delivered cost of a stable package operation: film usage, conversion yield, machine speed, scrap, rework, downtime, product loss from leaks, and the risk of premature shelf-life failure. A lower-cost roll that creates inconsistent pouch output may be more expensive than a structure with a higher purchase price but better operating margin.
A practical decision sequence
Selection becomes clearer when barrier, sealing, and speed are treated as linked constraints. First define the product protection requirement and the failure modes that cannot be tolerated. Then establish the pouch format and line conditions that determine how the web must behave. Screen material families against those needs, but reserve final approval for finished-pouch trials that include realistic sealing, filling, and handling conditions.
The strongest option is usually not the structure with the most impressive individual material claim. It is the one whose barrier remains appropriate after conversion and flexing, whose sealant operates reliably within the available process window, and whose web runs predictably at the output rate the business needs. That is the standard technical evaluators should use when comparing flexible packaging solutions for pouch packaging.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
