
Cardboard Grades Explained for Buyers: Strength, Finish, and End-Use Differences
Cardboard grades are best understood as combinations of fiber composition, construction, weight, stiffness, surface treatment, and resistance to handling conditions. Two sheets can look similar in a sample book yet behave very differently after printing, die-cutting, folding, stacking, or exposure to humidity. Grade selection therefore starts with the function of the finished pack: protect a product in transit, present it on a shelf, carry food, hold its shape after conversion, or provide a clean printed surface.
“Cardboard” is a broad commercial term rather than a single material. It commonly includes solid paperboard used for cartons and covers, as well as corrugated board used for shipping cases. The distinction matters because a heavier solid board is not automatically a substitute for corrugated board, and a smooth carton board is not automatically suitable for a moisture-prone distribution environment.
Begin with the job the board must perform
A useful first separation is between packaging presentation and transport protection. Folding carton grades are engineered to print, crease, and form neatly into retail cartons. Corrugated grades create spacing between liner sheets through fluting, which gives the board bending stiffness and cushioning. Paperboard for rigid boxes, dividers, backing cards, and industrial pads occupies the space between those two uses.
Failure often comes from specifying one visible property while overlooking the use condition. A bright white board can carry strong graphics but crack at a tight fold if its grain direction, caliper, and crease rule are mismatched. A robust corrugated case can perform well in a dry warehouse but lose compression performance after sustained exposure to humid air. A board that feels stiff as a flat sheet may still make a weak carton if the folds are repeatedly opened or if the glue area is poorly matched to its surface.
Folding carton board: finish, fold, and print behavior
Folding carton board is supplied as a flat, relatively dense sheet and is converted through printing, die-cutting, creasing, folding, and gluing. It is common where graphics, precise panel geometry, and a compact retail form matter. The relevant differences are often found in the board’s layers rather than its overall appearance.
Solid bleached sulfate board
Solid bleached sulfate, often shortened to SBS, is made largely from bleached virgin fiber. Its white interior and exterior support high-quality color reproduction, fine text, and clean visual contrast. It is frequently selected for premium printed cartons, cosmetic packaging, healthcare-related cartons, and other packs where both sides of the board may be visible.
Its printing surface is a major advantage, but surface quality should not be confused with structural capacity. A coated SBS sheet can produce sharp images while still requiring the right caliper for a tall carton, a heavy product, or a large unsupported panel. Crease performance also changes with board thickness and coating level. Deep scores, overly tight folds, or folds across an unfavorable grain direction can disrupt the surface and expose a light-colored crease line.
Folding boxboard
Folding boxboard, or FBB, is commonly built with mechanical pulp in its middle layers and lighter, cleaner fiber on the outer faces. This construction gives good stiffness relative to its basis weight, which is valuable when a carton needs rigidity without excessive material mass. It is widely used for consumer goods cartons, sleeves, and multipack structures.
The central layers contribute bulk, so caliper alone does not reveal all of the board’s behavior. A bulky sheet can resist bending well, yet its cut edges, embossing response, and fold appearance should be evaluated with the intended tooling. When a design relies on intricate windows, narrow tabs, or very small locking features, the board’s internal structure and die-cut quality become as relevant as its stated weight.
Coated recycled board
Coated recycled board, often called CRB or white-lined chipboard in some markets, uses recycled fiber and usually presents a coated white printing side with a darker reverse. It is suited to many cartons where a polished outer panel is needed but the inside of the pack is not part of the visual experience. Product contact, odor sensitivity, and required barrier performance need separate review rather than being inferred from the printed face.
Recycled content can create more variation in shade, surface uniformity, and edge appearance than premium virgin-fiber grades. That does not make the material unsuitable; it changes the tolerances that matter. Large areas of pale ink, uncoated graphic effects, exposed edges, or reverse-side printing deserve physical samples from the actual proposed grade.
Uncoated kraft and unbleached carton board provide a more natural brown appearance and can offer durable fiber characteristics. They are often chosen when the pack design uses the substrate color as part of the visual language. Ink opacity, varnish selection, and color expectations need adjustment because the underlying brown tone influences the printed result.
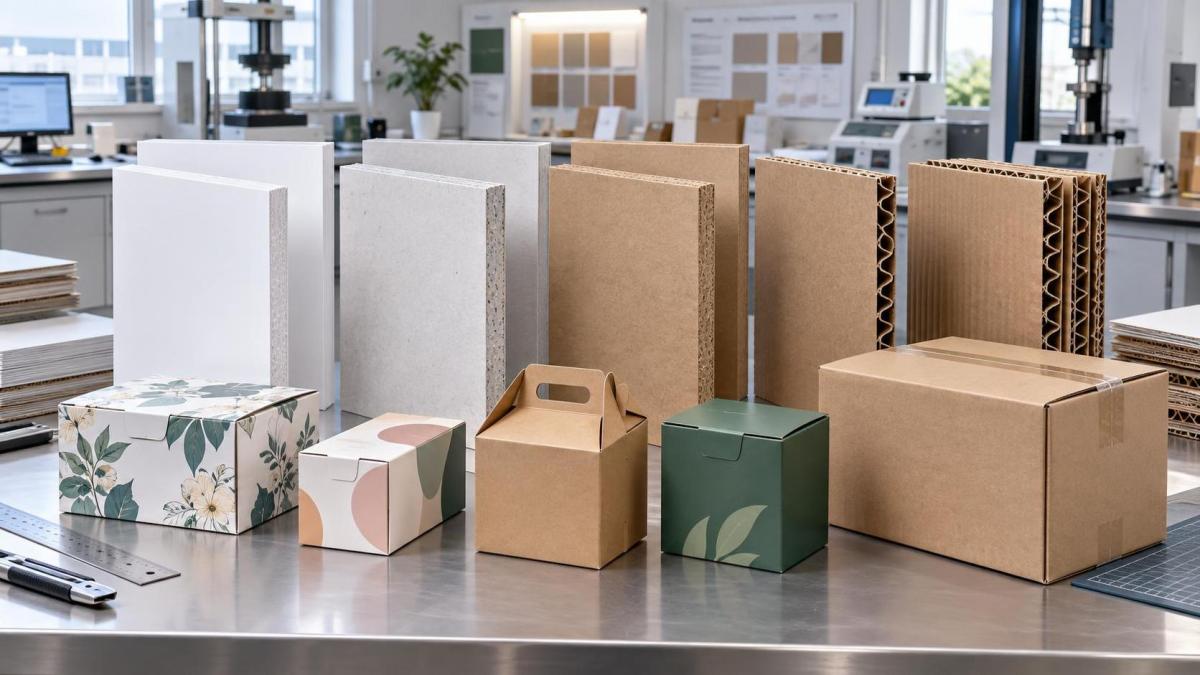
Corrugated grades: liners, flutes, and combined board
Corrugated board consists of one or more fluted mediums bonded to flat linerboards. The flutes form an arched structure that creates separation between the liners. This construction is why corrugated board can provide strong resistance to bending and compression without becoming a solid, heavy sheet.
A single-wall board has two liners around one fluted medium. Double-wall board uses three liners and two flute layers, while heavier multiwall constructions add further layers. More layers can increase protection and stacking capability, but they also affect thickness, weight, die-cutting behavior, storage volume, and the folding geometry of a case.
Linerboard choices
Kraft linerboard is commonly associated with strong virgin fibers and a brown exterior. It is widely used when transport durability and tear resistance are priorities. The familiar brown surface is printable, especially for simple graphics, but it does not reproduce fine images like a smooth coated carton board.
Test liner is generally made with recycled fiber and is used across many corrugated applications. Its performance varies by construction, fiber mix, and environmental conditions. A test liner specified only by appearance leaves too much unresolved; the relevant question is how the finished combined board performs in the intended box style and distribution environment.
White-top liner places a printable white surface on one side of a corrugated sheet. It offers a middle path where a shipping case also serves as a visible retail display or brand-facing outer pack. Its print result still depends on flute profile, liner smoothness, printing method, and whether graphics fall across broad panels, scored areas, or flaps.
Flute profile changes the result
Flutes are identified by profile families that differ in height and pitch. Larger flutes tend to provide more cushioning and separation between liners, while finer flutes create a thinner board with a smoother surface for printing and tighter folding. A fine flute may suit retail-ready packs and smaller die-cut structures; a larger flute is often better where impact protection or vertical compression is more important.
Choosing a flute solely by thickness is a common error. A taller profile may increase cushioning but produce wider score tolerances and more visible washboarding under graphics. A finer profile can improve the printed face, yet it may not provide the same resistance to crushing in demanding distribution. The geometry of the box matters too: long panels, heavy contents, hand holes, and stacked pallet loads impose different stresses than a small self-locking tray.
Strength terms that are often read too narrowly
Basis weight describes material mass per unit area. It is useful for consistency and cost comparison, but it does not independently predict package strength. Board composition, moisture level, caliper, flute structure, and pack geometry all influence the finished result.
Caliper is sheet thickness. Greater caliper can add rigidity and improve the feel of a carton, but it also changes the crease, fold, and glue-line behavior. On corrugated board, thickness largely reflects flute construction, which is why two boards with similar overall thickness can differ in compression and print surface.
Stiffness concerns resistance to bending. It is especially important for tall cartons, hanging packs, display panels, and large unsupported faces. Stiffness is directional: board bends differently with the machine direction than across it. Artwork placement and carton layout should recognize grain direction early, since changing the blank orientation late in production may change both fold quality and sheet yield.
Compression strength matters when cartons are stacked. It is a system property, affected by the board, box dimensions, score quality, closure design, product support inside the box, and ambient humidity. A compression value for a flat sample should not be treated as a guarantee of real stacking performance once the board has been printed, converted, stored, and assembled.
Puncture and tear resistance become important where edges, corners, or rough handling threaten the pack. These properties are relevant to corrugated shippers and industrial wraps, but a stronger liner cannot fully compensate for weak box design, poorly supported contents, or large empty voids inside a case.
Finish is a production variable, not only a visual choice
Coated board provides a smoother and more controlled surface for detailed graphics, dense solids, varnishes, and fine type. It can reduce ink absorption and improve apparent sharpness. Uncoated or kraft surfaces absorb more ink and retain visible fiber texture, which may suit a natural presentation but requires realistic color expectations.
Printing method changes the grade decision. Offset lithography benefits from a flat, stable sheet and is commonly associated with carton board or litho-laminated corrugated applications. Flexographic printing is widely used directly on corrugated linerboard and is well suited to transport packaging, although flute structure and liner smoothness influence detail. Digital processes introduce further considerations such as surface energy, toner or ink adhesion, curl, and variable-data placement.
After printing, coatings, lamination, foil, embossing, and heavy ink coverage can alter crease behavior. A finish that looks excellent before conversion may crack, scuff, or delaminate at folds if the board, coating, scoring rule, and folding sequence have not been tested as a set. Samples should therefore be converted in the intended sequence rather than evaluated only as printed flat sheets.
Moisture exposure changes the material equation
Paper-based board absorbs and releases moisture from surrounding air. As moisture rises, fibers soften and corrugated flutes can lose part of their load-bearing shape. In a dry environment, the same board can become more brittle and show different fold behavior. These shifts are especially important for cases that move between climates, spend time in chilled areas, or sit near loading docks.
Water resistance, grease resistance, vapor protection, and direct-contact suitability are separate properties. A moisture-resistant coating does not automatically establish grease resistance, and a barrier layer can complicate recycling, folding, adhesive selection, or print adhesion. The product, storage route, and disposal requirements should define the barrier need before a board grade is selected.
Where specifications become incomplete
A grade name alone is rarely enough for a release specification. “White carton board” does not state caliper, coating side, reverse-side requirement, grain direction, tolerance, fold performance, or acceptable shade variation. “Double-wall corrugated” does not identify flute combination, liner construction, box style, print surface, or the environmental conditions under which performance is expected.
- For folding cartons, record the board family, nominal basis weight or caliper, coated or uncoated faces, grain direction, printing process, finish, and the functional requirement at folds and glue areas.
- For corrugated packs, describe the combined board construction, flute profile or profiles, liner faces, case style, product mass and support, stack pattern, and expected handling environment.
- Where appearance matters, approve a physical standard that covers shade, gloss, reverse-side appearance, and the outcome after printing and converting rather than approving a bare board swatch.
Conversion details deserve the same attention as the board itself. Dull die-cutting rules can leave fuzzy edges or crush corrugated flutes. Poorly set crease rules can fracture coated carton surfaces or create loose folds. Adhesive performance depends on surface treatment, coating, dust, moisture, open time, and the pressure applied at the glue station. A material change that appears equivalent on paper can expose these differences immediately on a high-speed folder-gluer or case-packing line.
Comparing grades without relying on labels alone
Start with representative samples in the actual pack design. Print the relevant artwork, apply the intended finish, die-cut the blank, form the package, and assess it after realistic storage and handling. This sequence reveals interactions that separate laboratory sheet properties cannot show: score cracking after varnish, loss of case squareness, poor glue adhesion, visible flute texture, or reduced stacking performance after humidity conditioning.
For a retail carton, the decisive trade-off is often between a refined print surface and the stiffness needed to maintain the pack’s shape. For a shipping case, the issue is usually the balance between board construction, box geometry, product support, and moisture exposure. For food cartons or packs with a barrier requirement, the board grade must be considered together with the coating or laminate and the converting process.
The right grade is the one whose construction and finish match the finished package’s actual stresses. Treat board names as a starting point, then define the measurable properties, conversion conditions, and end-use environment that turn a material description into a reliable packaging specification.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
