
How to Evaluate a Corrugated Packaging Manufacturer for High-Volume Supply?
High-volume corrugated packaging failures rarely begin with an obviously bad box. They begin with a supplier whose quoted specification is too vague, whose capacity is measured in average output rather than available output, or whose quality system cannot keep board performance stable when paper grades, weather, order mix, or production load change.
For a large shipping program, the lowest quoted unit price can become the highest-cost option if it produces line stoppages, damage claims, excess void fill, rejected print, emergency freight, or repeated redesign work. A capable corrugated packaging manufacturer should therefore be assessed as a production and supply-chain partner: able to convert a defined packaging requirement into repeatable board, converting, inventory, and delivery performance at the required volume.
Start with the operating requirement, not the supplier’s standard box grade
A request for “double-wall cartons” or “32 ECT boxes” is not yet a complete high-volume specification. Those descriptions may be useful starting points, but they do not define the real demands placed on the packaging during filling, sealing, palletizing, warehousing, parcel handling, or long-distance transport.
The manufacturer should be able to translate the application into a documented technical brief. That brief should distinguish between the product weight and the load carried by the box; static stacking and dynamic transport loads; manual and automated packing; domestic and export distribution; humidity exposure; required shelf appearance; and any need for retail-ready print or consumer-facing claims.
For example, a carton that performs acceptably in a dry, short-distance pallet network may fail in a parcel channel where drops, conveyor compression, variable orientation, and high humidity reduce its effective safety margin. A supplier that responds only with a generic board grade, without questioning the distribution environment, is not providing enough technical assurance for a large-scale supply commitment.
Important points to define before comparing quotations include:
- Internal dimensions, dimensional tolerances, flute direction, and allowable variation after conversion.
- Board construction: liner and medium grades, flute profile, single-wall or double-wall configuration, and recycled-fiber content where relevant.
- Performance targets, such as edge crush, burst, puncture resistance, compression performance, or application-specific transit testing.
- Print method, color expectations, barcode readability requirements, artwork approval process, and acceptable cosmetic defects.
- Joint type, adhesive requirements, die-cut features, hand holes, perforations, moisture protection, and machine-erectability requirements.
- Pack-out quantity, pallet pattern, unit-load protection, delivery format, and warehouse handling constraints.
Performance metrics must not be treated as interchangeable. Edge Crush Test (ECT) evaluates resistance to edgewise compression of corrugated board and is often relevant to stacking strength. Burst strength measures resistance to rupture under pressure. Neither result alone proves that a finished case will survive a particular distribution cycle. Box geometry, score quality, moisture content, flute condition, pallet configuration, and load duration all influence actual performance.
Test whether capacity is truly available at the required service level
A manufacturer may operate a large corrugator and multiple converting lines yet still be unable to support a high-volume program reliably. Installed equipment capacity is not the same as available capacity. The relevant question is whether the supplier can produce the required mix of sizes, flute combinations, print treatments, and delivery frequencies without displacing the order when demand peaks or machinery is under maintenance.
Ask for a capacity discussion based on the specific program rather than a headline production figure. Relevant evidence includes the corrugator’s working width, compatible flute profiles, converting equipment, number of shifts, changeover intensity, storage limits, and the share of output already committed to other customers. A plant producing long runs of plain regular slotted cartons may have a very different effective capacity for short-run, multi-SKU, flexographically printed die-cuts.
High-volume supply also depends on bottlenecks beyond board-making. Die-cutting, flexographic printing, folding, gluing, bundling, palletizing, and dispatch can constrain throughput even if corrugated board is readily available. Where the program includes retail graphics or precise brand colors, print capacity and inspection capability deserve the same scrutiny as the corrugator.
Useful questions include whether the plant can run the specified work on more than one machine, what happens when a critical converter is unavailable, and whether tools, inks, and approved artwork are transferable between production locations. A second plant is not meaningful continuity protection if it cannot reproduce the same board configuration, print standard, tooling, and delivery format.
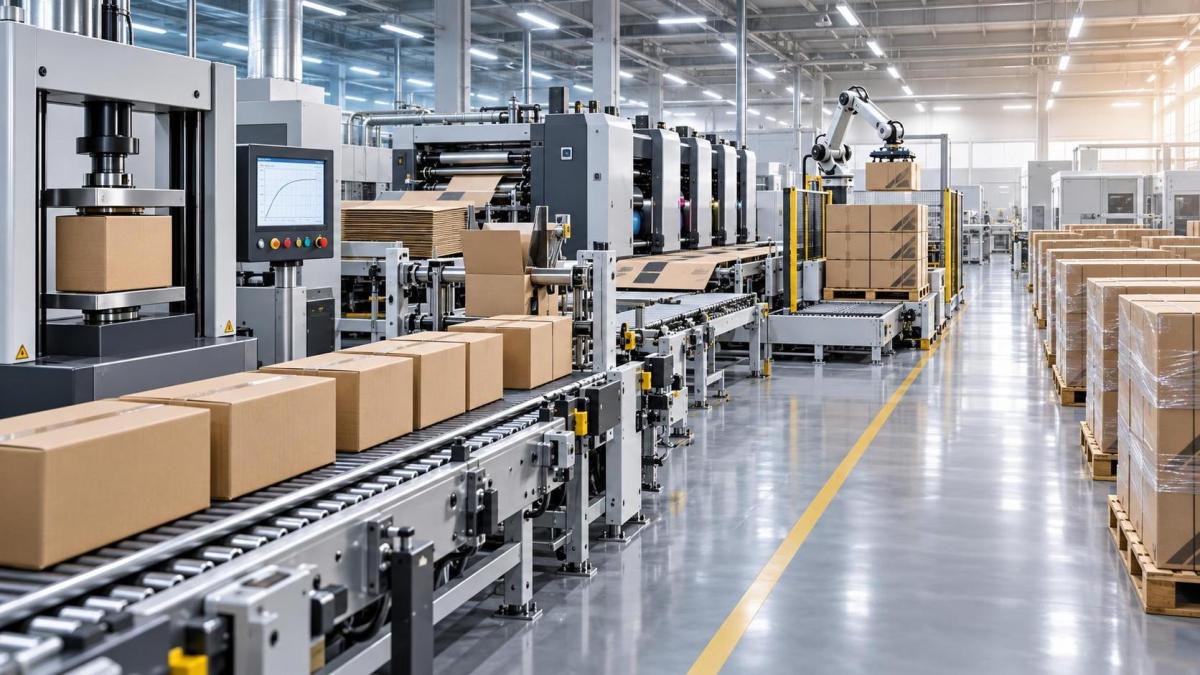
Examine board consistency at the point where it affects packaging cost
Corrugated packaging is a composite material. Its final performance is shaped by paper quality, adhesive application, corrugating conditions, moisture balance, flute formation, trimming, scoring, and conversion. Variation in any of these areas can increase waste on an automated packing line even when the finished cartons appear visually acceptable.
For high-volume programs, ask the manufacturer to explain its control plan from incoming paper through finished-goods release. This should cover how liner and medium are identified and controlled; how board caliper, bond quality, moisture, warp, and strength properties are monitored; how converting defects are classified; and how nonconforming material is segregated and traced.
Traceability should link a delivery batch to its production date, machine or line, relevant paper inputs, and inspection records. The purpose is not administrative formality. If a warehouse reports poor case squareness, weak joints, excessive warp, or barcode scan failures, traceability determines whether the issue can be isolated quickly or whether entire inventories must be treated as suspect.
Finished-case quality is especially important where cartons run through automated erectors, case packers, tape sealers, print-and-apply labeling systems, or robotic palletizers. Small differences in score depth, blank squareness, flap geometry, glue placement, bundle compression, and moisture can create jams or poor sealing. A manufacturer should be able to provide samples produced on normal commercial equipment, not only hand-finished approval samples, and should support line trials under representative operating conditions.
Do not confuse a specification sheet with a validated packaging design
Many cost problems arise because the quoted board grade was selected by precedent rather than by design validation. A box can be over-specified in one property and under-protected in another. Raising board weight may increase material cost without solving a failure caused by poor dimensions, weak score design, inadequate pallet pattern, or unsuitable closure.
The stronger manufacturer will discuss the complete load path: how the product is supported inside the case, how loads transfer through the flutes and corners, how the case behaves after sealing, and how pallet stacking changes compression exposure. If the packaging carries heavy products, fragile goods, liquid containers, or items with uneven load distribution, this discussion should include internal fit and any need for inserts, pads, partitions, or redesigned geometry.
Transport testing may be appropriate when the failure consequence is material or when the distribution environment is severe. The test method should be agreed in advance and reflect actual handling risks. It is not enough to say that a box “passed testing” without identifying the sample condition, conditioning environment, test sequence, acceptance criteria, and whether the tested design matches production material.
There is also a commercial reason to validate early. Once printing plates, die-cut tooling, inventory policies, warehouse procedures, and customer operations are built around a carton design, changes become slower and more expensive. Design work before contract award can prevent later disputes over whether a defect originates in the box, the packed product, the packing process, or transport conditions.
Assess printing and conversion as separate manufacturing risks
For plain transit cases, print may be limited to identification marks and handling instructions. Even then, barcode placement, contrast, ink rub resistance, and legibility after warehouse handling can matter. For branded e-commerce cartons or retail-facing corrugated packs, print quality becomes a formal part of supply performance.
Clarify the required print process and realistic expectations for it. Flexographic printing is widely used for corrugated packaging and can be highly effective, but color matching, fine type, screens, registration, and appearance depend on board surface, plate condition, press capability, ink system, and run conditions. A proof approved on one substrate or production method should not be assumed to predict every production result.
The supplier should define an artwork-control process covering approved files, version control, plate ownership, color targets where needed, first-run approval, retention samples, and procedures for artwork changes. For regulated products or controlled distribution channels, incorrect text, symbols, or codes can be more serious than a cosmetic defect. Controls must address content accuracy as well as print appearance.
Conversion quality also deserves explicit acceptance criteria. Cracked scores, incomplete cuts, loose waste, crushed flutes, poor glue joints, misaligned hand holes, or inconsistent perforations can impair packing operations and reduce compression performance. Broad language such as “good commercial quality” leaves too much room for disagreement when volumes are large.
Calculate total landed packaging cost, not only the ex-works carton price
The financial comparison should extend beyond the price per thousand units. Corrugated packaging has a large physical footprint, so freight, pallet utilization, warehouse space, and delivery frequency can materially change the effective cost. A lower factory price may be offset by low pallet density, long replenishment cycles, higher minimum order quantities, or the need to carry excess inventory.
A practical cost model should include quoted box price, tooling and artwork charges, freight and accessorial charges, packaging of the packaging, inventory carrying cost, expected obsolescence exposure, quality-related waste, line efficiency effects, damage-related costs, and the cost of expedited replenishment. This is particularly important when an apparent material downgrade produces more damaged shipments or when a lower-cost supplier requires larger and less flexible order releases.
Price adjustment mechanisms require equal attention. Paper is a major cost component of corrugated packaging, and a transparent agreement should state the reference basis, adjustment frequency, included paper grades, conversion element, freight treatment, and notification process. A vague “paper surcharge” clause makes budgeting difficult and can obscure whether changes reflect documented input movements or discretionary pricing.
Where annual demand is uncertain, the contract should separate forecast volumes from firm releases. This avoids treating a planning estimate as an unconditional purchase commitment while still giving the manufacturer enough visibility to reserve paper, capacity, and storage. Forecast accuracy, frozen periods, lead times, and cancellation rules should be matched to the supplier’s material purchasing and production realities.
Supply resilience is a measurable requirement
High-volume corrugated supply is exposed to paper availability, transport disruption, energy interruptions, equipment failures, labor constraints, and demand spikes. Resilience should be evaluated through operating arrangements rather than broad assurances about reliability.
Determine how many qualified paper sources support the specified board construction, whether equivalent grades require reapproval, how safety stock is held, and who owns it. Supplier-held inventory can improve responsiveness, but it should be clear whether it is dedicated stock, shared stock, finished cartons, board, or raw paper. Each option carries different risks of obsolescence and different response times.
Delivery performance should be defined with precision: requested delivery date, permitted delivery window, minimum drop size, incomplete-shipment rules, damage reporting, pallet labeling, and delivery-document requirements. A useful service measure distinguishes a complete, correctly identified, undamaged delivery from a shipment that merely left the factory on time.
Business continuity planning should also cover practical alternatives. Can approved artwork, plates, dies, and specifications be accessed if the primary site is unavailable? Can a secondary facility make an equivalent product? How is approval managed if paper or ink substitutions become necessary? A continuity plan is credible only when the alternative route has compatible equipment and documented technical controls.
Verify sustainability and compliance claims against the product and destination
Environmental claims should be tied to evidence rather than broad statements about paper packaging. If chain-of-custody certification is required, certifications such as FSC or PEFC may be relevant, but the claimed status of the delivered product must align with the supplier’s current certification scope and documented claim process. Certification alone does not establish recycled content, recyclability in every local system, or suitability for food contact.
Food, pharmaceutical, cosmetic, and other sensitive applications require more detailed review. Food-contact suitability may involve the board, inks, coatings, adhesives, recycled-fiber content, intended use, and whether a functional barrier separates packaging from the product. Requirements vary by market and application. A general declaration should not replace a product-specific compliance review where the carton may contact food directly or indirectly.
For export programs, confirm country-of-origin documentation, wood-free pallet requirements where applicable, labeling language, restricted-substance declarations, and any customer-specific packaging standards before tooling is released. Compliance obligations should be written into the specification and change-control process; they should not sit only in email correspondence or artwork notes.
Use the supplier qualification process to expose execution gaps
Samples, quotations, and factory audits are most valuable when they test the same risks that will exist after launch. A qualification process should compare commercial samples with production-run material, verify critical dimensions and performance attributes, assess packaging-line compatibility, and establish release criteria before volume orders begin.
Contract terms should identify ownership and maintenance responsibilities for dies and printing plates; procedures for specification changes; batch identification; inspection rights; complaint handling; corrective-action expectations; and remedies for recurring nonconformance. These provisions are not substitutes for supplier capability, but they reduce ambiguity when operational pressure is highest.
The right corrugated packaging manufacturer is not necessarily the one offering the heaviest board, the newest equipment, or the lowest nominal price. It is the supplier that can demonstrate repeatable performance for the actual distribution system, protect capacity for the required order pattern, explain how quality is controlled, and make the cost and risk assumptions visible before the first large release is placed.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
