
What Corrugated Packaging Evaluation Services Should Verify Before Product Launch?
Corrugated packaging evaluation services should establish whether a pack will remain functional from converting through distribution and opening, under the actual conditions it will face. A board sample that appears strong on a bench can still fail after die-cutting, printing, filling, pallet stacking, humidity exposure, vibration, or repeated handling. Pre-launch verification therefore needs a linked view of material, structure, process capability, and applicable compliance evidence.
The central question is whether the finished pack protects its contents with sufficient consistency, rather than whether an individual blank passes a single strength test. Evaluation should begin with the product mass, dimensions, center of gravity, fragility, closure method, expected stacking pattern, handling route, storage climate, and intended pack orientation. These inputs determine which properties need priority and which test result could be misleading when viewed alone.
Confirm the board specification behind the sample
Corrugated board should be identified by construction, not only by its nominal grade or visual appearance. The evaluation record should distinguish liner and medium types, flute profile, board combination, adhesive system, basis weight tolerances, caliper, and any coating or print surface treatment. A change in any of these elements can alter compression behavior, crease quality, moisture response, print receptivity, and die-cut performance.
Board caliper is frequently overinterpreted. A thicker sheet may offer useful cushioning or panel stiffness, yet thickness alone does not prove higher stacking strength. Flute geometry, liner stiffness, bonding quality, moisture content, and the loss of material at creases all affect the finished box. Conversely, a thinner design with suitable liners and well-controlled converting may perform better than a thicker board that has weak bonding or poor score formation.
Fiber composition and recycled content should be assessed against the intended duty cycle. Recovered fiber can perform well in many applications, but its response to repeated moisture exposure, long storage, or high compression loads should be supported by relevant evidence. Where a pack is exposed to refrigeration, coastal transport, unprotected loading bays, or humid warehousing, conditioning and testing should reflect those conditions rather than relying on dry-state data.
Bond integrity deserves separate attention. Weak adhesive bonds between liner and medium can produce localized flute separation, soft panels, or reduced resistance near scores and cutouts. These defects may not be obvious before conversion. Evaluation should inspect bond uniformity across the sheet and near the locations where the design places stress, including hand holes, locking tabs, glue flaps, and narrow bridges between die-cut features.
Translate product loads into a defensible box design
Packaging drawings should be reviewed as load-bearing structures. Internal dimensions must accommodate the product and any inserts without forcing panels outward. Excess free space creates impact movement; an overly tight fit can deform the carton during filling, weaken closure engagement, or transfer compression directly to a sensitive product.
Panel geometry is especially important for regular slotted cartons, wraparound cases, trays, and shelf-ready formats. Compression is carried primarily through vertical corners when the box is properly erected and loaded. Long unsupported panels, oversized access openings, deep scores, perforations, and large printed windows can interrupt that load path. A design can retain a favorable board-strength value while losing practical stacking performance because the converted geometry concentrates stress in weakened areas.
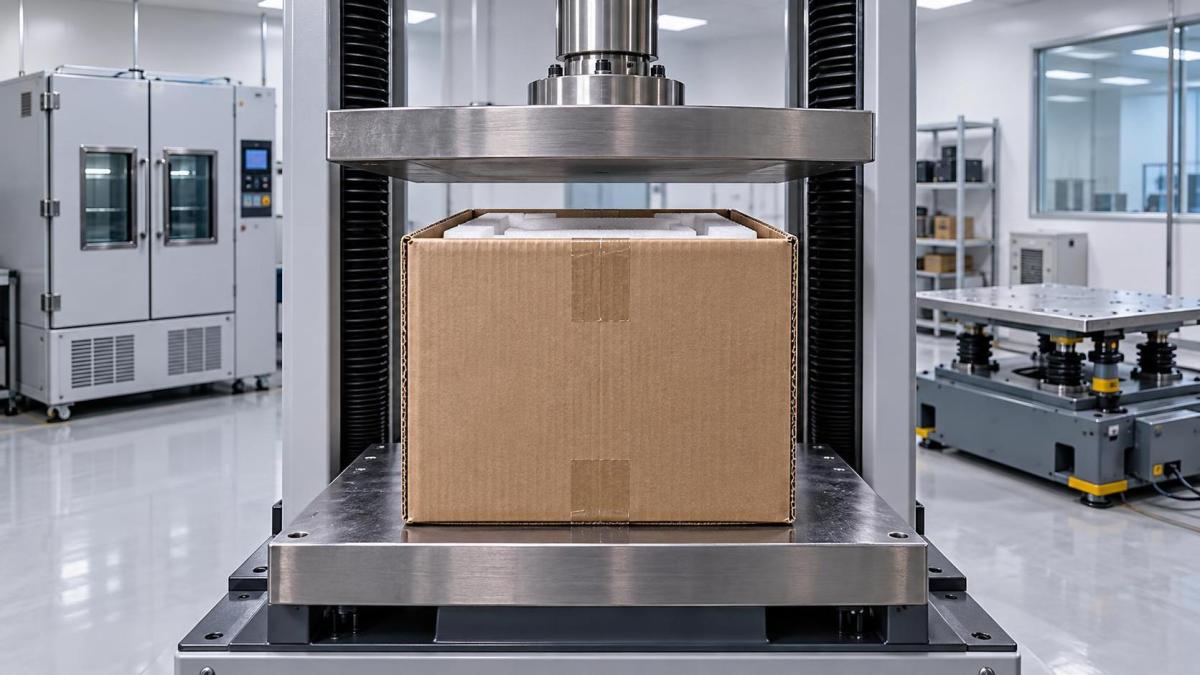
Evaluation should examine the relationship between product weight and the stacking scenario. The relevant load is not simply the weight of several filled boxes multiplied together. Pallet overhang, uneven unit loads, warehouse dwell time, strap or stretch-film pressure, pallet deck gaps, and transport acceleration can introduce localized forces. Boxes near the bottom of a stack may also absorb moisture or suffer corner damage before the compression event occurs.
Where the product has a high center of gravity, irregular footprint, or rigid corners, the package should be assessed for concentrated loading. A heavy item resting against one panel can bow the board during transport and loosen a closure. Internal fitments, pads, partitions, or orientation controls may be needed, but they should be tested as part of the complete system. An insert that looks protective in isolation can cause a carton to bulge, reduce stacking contact at corners, or abrade a printed surface.
Use tests that reproduce the failure mechanism
Material tests provide useful screening data, but they do not replace package-level verification. Edgewise board properties can indicate potential compression performance, while bursting resistance addresses a different failure mode. Neither result alone confirms that a specific box will survive its route. The service scope should connect each test to a known or plausible hazard.
Testing should include representative filled packs rather than empty cartons whenever product interaction influences the result. Empty boxes can reveal board collapse or poor erection, but they cannot show internal movement, abrasion, product-to-panel pressure, or the way a heavy item changes the carton’s impact orientation. Representative contents should match mass distribution and surface characteristics, not just total weight.
Drop testing is most useful when it documents the chosen sequence and the observed damage mechanism. A corner impact may crush a load-bearing post; an edge impact may split a manufacturer’s joint or open a glued seam; a face impact may damage the contents without visibly harming the carton. The pass criteria should distinguish cosmetic scuffing from loss of containment, unsafe sharp edges, unreadable mandatory information, impaired product function, or compromised tamper evidence.
Vibration evaluation often identifies problems missed by a single-impact test. Repeated movement can cause contents to settle, tabs to work loose, dividers to migrate, and uncoated print areas to rub against adjacent packs. The packing arrangement used during the test matters. A carton that is stable when tightly packed on a test pallet may experience more movement when mixed with smaller or lower cartons in real distribution.
Inspect converting quality as a performance variable
Corrugated packaging is altered substantially during printing, die-cutting, scoring, folding, and gluing. Evaluation should inspect production-intent samples from the planned equipment and process settings where possible. Hand-made mock-ups are valuable for design development but often conceal limitations that emerge at production speed.
Scores need to fold cleanly without cracking liners, crushing flutes excessively, or causing panels to spring open. Poor score depth can produce distorted box geometry and reduce the contact between flaps. Over-scoring weakens the board along a line that may carry compression loads. Under-scoring makes erection inconsistent and can cause folding equipment to force the board, leading to random cracking or misalignment.
Die-cut features require similar scrutiny. Narrow tabs, small locking slots, tear strips, perforations, and hand holes are sensitive to registration and cutting variation. Excessive cut pressure may crush nearby flutes; insufficient pressure can leave tags that disrupt folding or create unsafe rough edges. The evaluation should verify that functional features work across samples taken from different positions in the sheet or production run, since variation can be directional.
For glued designs, adhesive type, application pattern, open time, compression during setting, and substrate surface condition all influence bond reliability. A joint may appear closed immediately after packing while retaining insufficient fiber tear or bond development for distribution. Coatings, dust, low surface energy treatments, and excessive moisture can alter adhesion. The review should capture the approved glue area and reject conditions such as skips, squeeze-out that contaminates contents, or adhesive placement too close to a score.
Verify print, identification, and pack communication
Print verification extends beyond color appearance. Essential markings must remain legible after conversion and expected handling. Barcodes, batch areas, orientation arrows, recycling marks, hazard communication, and handling instructions should be reviewed on the actual corrugated surface, after any varnish or coating, rather than only on an artwork proof. Flute direction and board roughness can affect ink coverage, fine type, line sharpness, and code scanning.
Color approval should account for the intended substrate and viewing conditions. A design approved on a smooth proof may shift visibly on a mottled recycled liner or after a coating changes gloss. Registration matters where graphics align with die-cut windows, embossed effects, or fold lines. Even small movement can place text too close to a score, leave a graphic partly hidden after erection, or expose an unintended white edge.
Rub resistance should be evaluated when packs contact each other, slide on conveyors, or move through automated handling. Surface scuffing is not always a cosmetic issue: it can reduce barcode readability, obscure product identification, or transfer ink to adjacent packs. Where packaging contacts food, cosmetics, pharmaceuticals, or other regulated contents, the evaluation should confirm that the selected inks, coatings, adhesives, and substrate arrangement are supported by the applicable product-contact requirements. A generic statement that materials are “safe” is not a substitute for documentation linked to the specific use, temperature, contact side, and migration pathway.
Control moisture, storage, and release evidence
Moisture is one of the most consequential variables in corrugated performance. Elevated humidity can soften fibers, reduce compression strength, increase warp, weaken some adhesive bonds, and change tape adhesion. Very dry conditions can make liners more prone to cracking at scores. Evaluation should define the conditioning state of test samples and record it with the results; otherwise, later comparisons between suppliers, production lots, or laboratories can be unreliable.
Storage time also changes the question being answered. A newly converted carton may perform acceptably, while a box stored for an extended period under load shows creep, panel bowing, or gradual loss of closure integrity. Where launches involve prebuilt inventory or long distribution routes, retained samples and aging observations provide more useful release evidence than a fresh-sample result alone.
The final evaluation file should link the approved drawing, material specification, artwork revision, test configuration, conditioning details, sample identification, observations, and acceptance criteria. It should also state what changed from the evaluated sample to the released production pack. Board substitution, flute-direction changes, altered print coverage, revised cutouts, adhesive changes, or different product fitments can invalidate prior conclusions even when the external carton dimensions remain the same.
A disciplined release decision recognizes that corrugated packaging performance is a system outcome. The most reliable evidence comes from matching the board, conversion method, filled configuration, environmental exposure, and distribution hazards to the pack that will actually enter the market.
Related News
Get weekly intelligence in your inbox.
No noise. No sponsored content. Pure intelligence.
